Quick Answer
Spirits closure matching with CAD drawings and bottle samples helps buyers confirm whether a stopper, screw cap, ROPP cap, or specialty closure will fit and seal before bulk production. CAD drawings show target dimensions such as neck finish, bore ID, finish height, thread profile, and closure clearance. Physical bottle samples confirm real-world tolerance, insertion force, torque, leakage risk, visual balance, and production compatibility.
For custom spirits projects, closure matching with CAD drawings and physical samples gives buyers a safer way to confirm fit before approving tooling, decoration, or bulk production.
Why Closure Matching Matters Before Bulk Orders
Closure matching with CAD drawings and physical samples is the process of checking bottle neck dimensions, closure structure, material behavior, and real bottle fit before bulk production. For spirits brands, distilleries, private label buyers, importers, distributors, bottlers, and packaging buyers, this step can prevent expensive mistakes before bottles, closures, labels, capsules, cartons, and export shipments are confirmed.
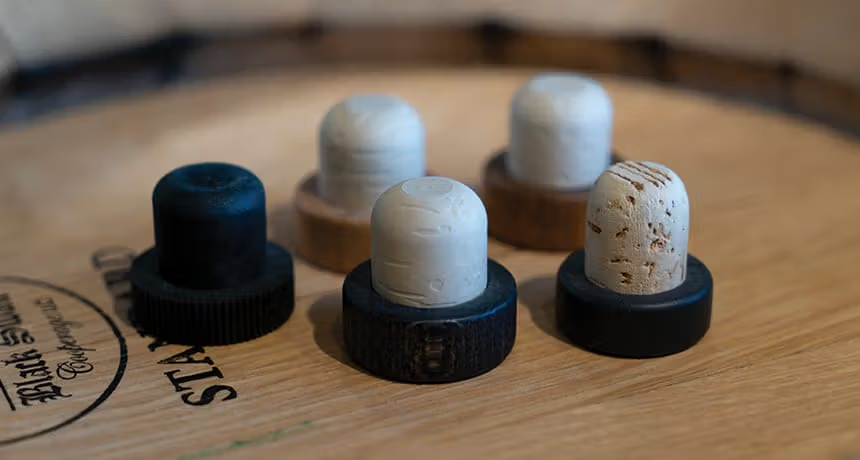
A spirits closure is not only a decorative component. It protects the liquid, supports brand positioning, affects the opening experience, and influences filling-line efficiency. A whiskey stopper, gin bottle cap, tequila cork closure, vodka screw cap, rum bar-top stopper, or liqueur ROPP cap must match the bottle, the spirit, the decoration system, and the production plan.
CAD drawings show the design target. Physical bottle samples prove the production reality.
A closure that looks correct in a catalog, rendering, or CAD file may still fail on the actual bottle. The stopper may be too tight, too loose, or visually unbalanced. A screw cap may cross-thread or fail to seal. A ROPP cap may not form correctly on the bottle finish. A capsule may interfere with the closure head. These issues are easier to prevent during sample review than to correct after bulk production.
If you already have a bottle drawing, neck finish data, closure reference, or physical bottle samples, Kandacork Closures & Stoppers can help review closure fit through its closure matching support before sample production or quotation.
Why CAD Drawings Alone Are Not Enough
CAD drawings are an essential starting point for closure matching. They help the supplier understand the intended bottle design before physical samples are tested. A technical drawing can show the bottle neck finish, outer diameter, inner bore, finish height, thread profile, ROPP finish, shoulder clearance, and decoration space.
For screw caps and ROPP caps, CAD drawings are especially important because the closure must engage, form, seal, or torque correctly. For bar-top stoppers, drawings help estimate shank diameter, insertion depth, head proportion, and possible capsule clearance.
A CAD drawing can help answer important questions:
- What closure family is suitable for this bottle?
- Is the bottle designed for a bar-top stopper, screw cap, ROPP cap, or specialty closure?
- What is the target bore diameter?
- Is there enough clearance for the closure head or capsule?
- Does the neck finish support the expected sealing method?
- Does the closure design look proportional to the bottle?
However, CAD drawings cannot confirm everything. They describe the intended design, not the final production result.
Real bottles may have small but important variations. The inner bore may be slightly larger or smaller than the drawing. The neck may be slightly oval. The inside wall may have a taper or pinch point. The glass surface may create more or less friction than expected. These details can change stopper insertion force, pull-out feel, leakage risk, cap torque, and final appearance.
This is why closure matching with CAD drawings and physical samples is more reliable than choosing a closure from a catalog or drawing alone.
For threaded closure systems, torque performance may also be part of technical review. ASTM International’s D2063/D2063M is commonly used as a reference for measuring torque retention properties of container and continuous-thread closure systems. For beverage packaging, closure qualification guidance also reflects the importance of consistent testing methods between suppliers, bottlers, and brand owners.
Key Neck Dimensions to Check
Bottle neck finish is the foundation of closure compatibility. Before selecting a stopper, screw cap, ROPP cap, or specialty closure, buyers should confirm the key neck dimensions from the bottle drawing or supplier specification.
| Dimension | What It Means | Why It Matters for Closure Matching |
|---|---|---|
| T dimension | Outer thread or finish diameter | Helps select screw cap or ROPP cap size |
| I dimension / Bore ID | Inner opening diameter | Critical for bar-top stopper and cork shank fit |
| H dimension | Finish height | Affects cap skirt, ROPP forming, and capsule clearance |
| Thread profile | Thread shape and pitch | Determines screw cap engagement and torque behavior |
| Sealing surface | Contact area for liner or closure | Affects leakage prevention |
| Bore depth | Usable insertion depth | Affects stopper seating height and pull-out feel |
| Shoulder clearance | Space below the neck finish | Helps avoid capsule, sleeve, or closure interference |
These dimensions are especially important when the project uses custom glass bottles, premium stopper heads, capsules, or automated filling equipment. A small dimensional difference can affect both technical performance and visual appearance.
For buyers who need more detail on finish dimensions and real bottle checks, Kandacork’s guide to spirits bottle neck compatibility and closure fit testing explains how bottle neck measurements affect stopper, screw cap, and ROPP closure performance.
Bar-Top Bore Diameter: The Detail Many Buyers Miss
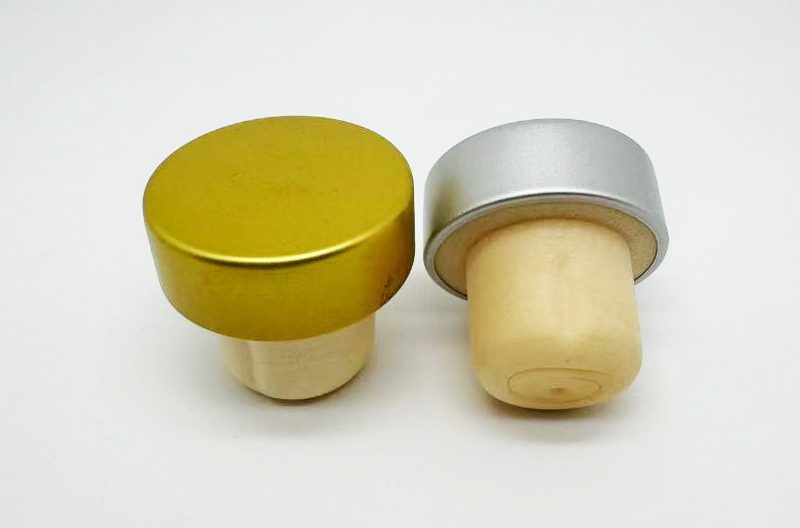
For bar-top stoppers, the inner bore diameter is one of the most important details. Unlike screw caps, bar-top stoppers do not rely on thread engagement. The shank must compress inside the bottle neck and create a secure, consistent fit.
If the bore is too narrow, the stopper may be difficult to insert or remove. If the bore is too wide, the stopper may feel loose, rise after insertion, or fail to seal properly. Even a small bore variation can change the final consumer experience.
This is why buyers should not approve a bar-top stopper based on one bottle sample only. For premium spirits stopper projects, Kandacork recommends checking several physical bottles before confirming the final shank diameter, shank material, or stopper structure.
For whiskey, rum, tequila, gin, brandy, and craft spirits, bore diameter affects more than sealing. It also affects the premium feel of the closure, the opening resistance, the seating height, and the way the closure aligns with the bottle.
Buyers comparing stopper formats can also review Kandacork’s article on how bar-top stoppers fit spirits bottle necks to understand how bore diameter, shank compression, and sample approval work together.
Example: When the Drawing Looks Correct but the Bottle Sample Changes the Decision
In a premium whiskey or rum project, the bottle drawing may show a bore diameter that appears suitable for a cork or synthetic shank. However, when several physical bottles are tested, one bottle may have a slightly tighter bore, inner taper, or higher surface friction. This can make the stopper difficult to insert or remove.
In this situation, Kandacork may recommend adjusting the shank diameter, testing another shank material, or reviewing bottle tolerance before approving bulk closure production. This is why closure matching with CAD drawings and physical samples is important before custom mold confirmation, decoration approval, or large-volume purchasing.
What Physical Bottle Samples Confirm
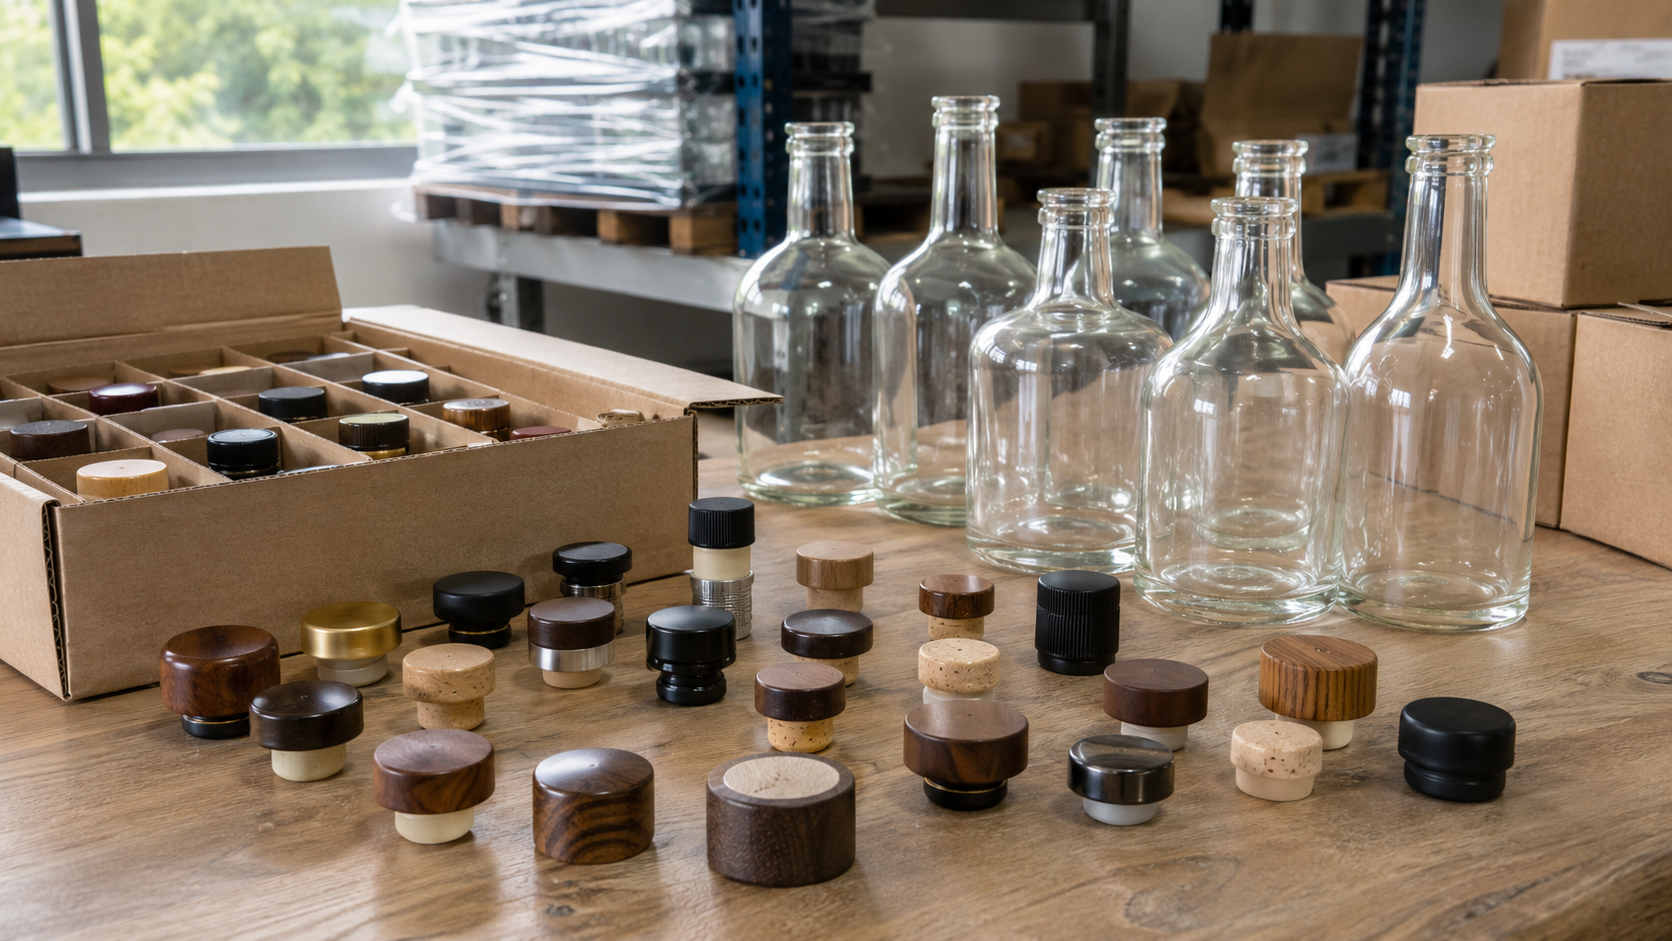
Physical bottle samples are necessary because the final closure must work with real bottles, not only with design files. Sample testing shows how the closure behaves during insertion, sealing, capping, decoration, storage, and transport.
For bar-top stoppers, physical sample testing should confirm:
- Shank insertion force
- Pull-out force
- Stopper seating height
- Seal contact
- Tightness consistency
- Risk of stopper rise
- Head alignment
- Consumer opening feel
- Visual balance with the bottle
- Compatibility with capsule or neck decoration
For screw caps, testing should confirm:
- Thread engagement
- Application torque
- Removal torque
- Liner compression
- Tamper-evident band behavior
- Cap skirt position
- Leakage risk
- Capping-line compatibility
For ROPP caps, testing should confirm:
- Correct cap size
- Bottle finish suitability
- Rolling and forming result
- Tamper-evident bridge performance
- Liner seal
- Removal behavior
- Capping equipment compatibility
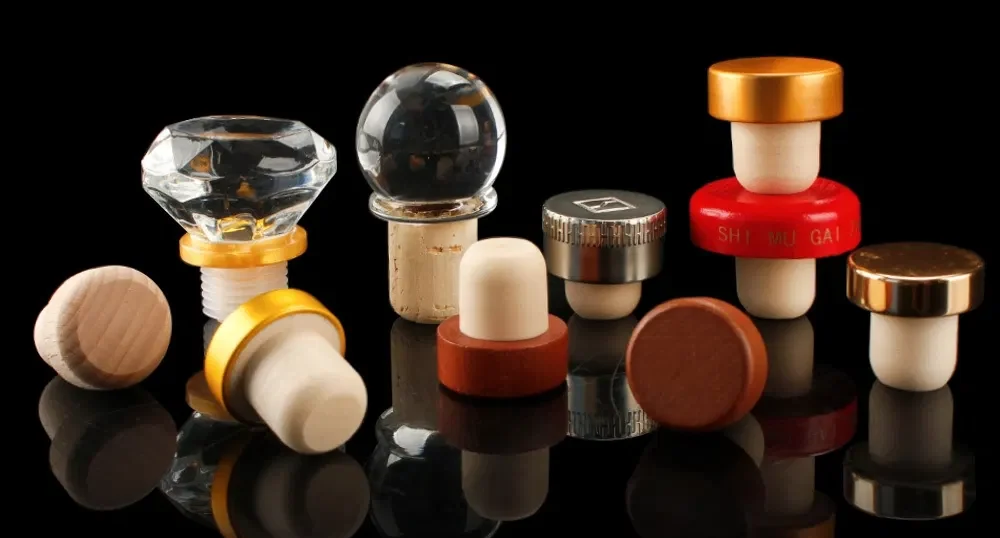
For premium glass stoppers or specialty closures, physical testing should also check seal structure, weight balance, handling safety, breakage risk, and export packaging stability.
Sample Review Tip:
For reliable closure matching, send 3–5 empty bottle samples, not just one. This helps Kandacork compare bore variation, stopper tightness, seating height, cap engagement, and visual balance before recommending a final closure size.
A practical sample package should include the bottle drawing, physical bottles, neck finish details, current closure reference if available, target spirit type, filling method, decoration plan, and expected order quantity.
CAD Review vs Physical Sample Review
The strongest closure matching process uses both CAD review and physical sample testing. Each step confirms different risks.
| Review Area | CAD Drawing Review | Physical Bottle Sample Review |
|---|---|---|
| Neck finish | Confirms design specification | Confirms actual production result |
| Bore diameter | Shows target size | Shows real tolerance and variation |
| Thread profile | Helps select screw cap type | Confirms real threading behavior |
| ROPP finish | Identifies cap direction | Confirms forming result |
| Stopper tightness | Can only estimate | Must be tested physically |
| Leakage risk | Limited prediction | Requires real sample testing |
| Capsule clearance | Can estimate by dimension | Must assemble to confirm |
| Visual balance | Can support rendering review | Real bottle assembly confirms appearance |
| Filling-line compatibility | Partial review | Requires trial or equipment data |
A drawing can reduce early uncertainty. A real sample confirms whether the closure works in practice.
For custom spirits stopper projects, Kandacork usually reviews the bottle drawing first, then checks the physical bottle samples before recommending the final shank size, closure structure, or cap specification. This helps avoid late-stage changes after mold development, decoration approval, or bulk purchasing.
Closure Matching Matrix for Spirits Packaging
Different spirits projects require different closure matching priorities. A closure that works for a vodka bottle may not be suitable for a premium whiskey bottle. A tequila stopper may need different sealing behavior from a liqueur screw cap.
| Spirits Project | Common Closure Type | What to Verify |
|---|---|---|
| Whiskey | Bar-top stopper, wood head stopper | Bore fit, pull-out force, premium feel, head proportion |
| Vodka | Screw cap, ROPP cap | Thread engagement, torque, liner compression, tamper evidence |
| Tequila | Cork stopper, synthetic stopper | Seal stability, stopper tightness, export handling |
| Rum | Bar-top stopper | Seating height, head alignment, shipping stability |
| Gin | Bar-top stopper, screw cap | Decoration balance, neck clearance, closure appearance |
| Brandy | Glass stopper, cork stopper | Luxury appearance, seal consistency, handling safety |
| Liqueur | Screw cap, bar-top stopper | Leakage risk, liner compatibility, reseal performance |
| Private label spirits | Cork, synthetic, screw cap, ROPP | Cost control, MOQ, fast sampling, repeatability |
This matrix helps buyers avoid choosing closures only by appearance. The right closure must match the bottle neck, product category, brand position, filling process, and distribution route.
For buyers still comparing closure families, Kandacork’s overview of bar-top stoppers vs screw caps vs ROPP closures for spirits can help narrow the technical direction before requesting samples.
Common Closure Matching Problems and Solutions
Most closure failures are easier to prevent before production than to fix after bulk goods are finished. The following table shows common problems, likely causes, and practical corrective actions.
| Problem | Possible Cause | What to Check | Recommended Action |
|---|---|---|---|
| Stopper too tight | Bore ID too small or shank oversized | Measure several bottle samples | Use smaller shank or different material |
| Stopper too loose | Bore ID too large or poor compression | Pull-out force and seal contact | Increase shank size or adjust material |
| Stopper sits too high | Bore depth too shallow or shank too long | Insertion depth and seating height | Modify shank length |
| Stopper rises after insertion | Compression rebound or pressure change | Filled sample and storage test | Adjust shank material or diameter |
| Leakage in transit | Poor seal contact or liner mismatch | Leak test and packing review | Improve seal design or liner |
| Cap cross-threading | Thread mismatch or poor alignment | Thread drawing and cap trial | Adjust cap specification |
| ROPP cap not forming | Wrong finish or capping setting | Bottle finish and capping trial | Confirm ROPP cap and equipment setup |
| Capsule interference | Closure head or skirt too large | Neck and shoulder clearance | Adjust head size or capsule design |
| Closure looks unbalanced | Head size not proportional | Real bottle assembly | Revise head diameter or height |
These issues may be caused by bottle tolerance, closure size, material behavior, decoration design, or production equipment. A good supplier should help identify the cause instead of only offering another standard closure size.
What Buyers Should Send for Sample Review or Quotation
A complete RFQ package helps the supplier recommend a better closure solution and prepare a more accurate quotation. It also reduces back-and-forth communication during sample development.
Kandacork can start the review with a PDF technical drawing, CAD file, bottle neck drawing, bottle photos, existing closure sample, or physical bottle samples. If the CAD file is incomplete, physical samples and measured bore data can still help the team recommend a sample direction.
Before requesting samples or pricing, buyers should prepare:
| Information to Send | Why It Matters |
|---|---|
| Bottle CAD drawing or technical drawing | Helps review neck finish, bore, height, and closure clearance |
| Physical bottle samples | Confirms real fit, tolerance, and appearance |
| Neck finish code | Helps select screw cap, ROPP cap, or stopper direction |
| Inner bore diameter | Critical for cork, synthetic, and bar-top stopper fit |
| Bore depth | Affects insertion depth and seating height |
| Existing closure reference | Helps compare size, material, and fit target |
| Spirit category and ABV | Supports material and sealing review |
| Filling and capping method | Helps check production compatibility |
| Decoration file or logo artwork | Supports printing, engraving, embossing, or color matching |
| Quantity and launch schedule | Helps estimate MOQ, lead time, and production plan |
| Destination market | Helps review export packing and documentation needs |
If some information is not available, buyers can still begin with bottle photos, basic measurements, and project goals. However, CAD drawings and physical samples will make closure matching more accurate.
For food and beverage packaging, buyers may also need to consider food-contact expectations. The FDA and EU Regulation (EC) No. 1935/2004 are useful reference points when reviewing materials intended to come into contact with food or beverage products.
Ready for Sample Review?
Send Kandacork your bottle CAD drawing, neck finish details, bottle photos, existing closure reference, or 3–5 physical bottle samples through the custom closure quote and inquiry page. The team can help review fit risks, recommend a closure direction, and prepare a sample or quotation plan before bulk production.
How to Evaluate a Closure Matching Supplier
A closure supplier should not be evaluated only by price. In spirits packaging, supplier capability directly affects launch timing, fit accuracy, quality consistency, and after-sale risk.
A qualified closure matching supplier should be able to:
- Read bottle CAD drawings and technical drawings
- Understand neck finish, bore diameter, and bottle tolerance
- Recommend suitable shank diameter, cap type, or closure structure
- Compare cork, synthetic, aluminum, plastic, glass, or specialty components
- Test closures with real physical bottle samples
- Identify fit risks before bulk production
- Support logo, color, texture, and decorative finish development
- Explain MOQ, tooling cost, sample cost, lead time, and quotation terms
- Maintain consistency for repeat orders
- Support export packing and shipment requirements
For premium bar-top stoppers, Kandacork recommends testing several bottles instead of relying on one sample. For unclear neck tolerance, sample fit testing should happen before mold confirmation. For screw caps and ROPP caps, the bottle finish, liner, torque, and capping process should be reviewed together.
Kandacork Closure Matching Workflow
Kandacork Closures & Stoppers supports spirits buyers through a practical matching process:
- Project Review
The buyer sends drawings, bottle photos, physical samples, or existing closure references. - Technical Assessment
Kandacork reviews the neck finish, bore diameter, closure type, material direction, and possible fit risks. - Sample Recommendation
Suitable closure structures, shank sizes, cap types, materials, and decoration options are recommended. Buyers can also explore Kandacork’s wider range of custom spirits closures and stoppers when comparing bar-top stoppers, screw caps, ROPP closures, and specialty systems. - Physical Fit Testing
Samples are checked with real bottles to review tightness, seating height, sealing contact, appearance, and handling feel. - Quotation and Production Planning
After sample direction is confirmed, Kandacork prepares quotation details including MOQ, unit price, tooling cost, lead time, packing, and production plan.
This workflow helps buyers move from research to inquiry and from inquiry to production with lower technical risk. For projects that also require bottle sourcing, decoration, and export-ready coordination, the wider Kandacork group can support complete spirits packaging through custom glass bottles, closures, and decoration.
Frequently Asked Questions
What is closure matching with CAD drawings and physical samples?
Closure matching with CAD drawings and physical samples is the process of checking bottle dimensions, closure structure, material behavior, and real bottle fit before bulk production. CAD drawings help review technical dimensions, while physical samples confirm actual fit, sealing, appearance, and handling performance.
Can CAD drawings confirm closure fit?
CAD drawings can confirm important design details such as neck finish, bore diameter, finish height, thread profile, and closure clearance. However, they cannot fully confirm real bottle tolerance, insertion force, leakage risk, or consumer opening feel. Physical sample testing is still recommended.
Why are physical bottle samples necessary?
Physical bottle samples are necessary because real bottles may differ slightly from the drawing. Bore diameter, inner taper, neck roundness, glass surface, and production tolerance can all affect stopper fit, cap torque, sealing performance, and final appearance.
How many bottle samples should buyers send?
For reliable closure matching, buyers should send 3 to 5 empty bottle samples when possible. If bottles from different production batches are available, they are useful for checking tolerance variation before confirming the closure specification.
What dimensions are needed for spirits closure matching?
Important dimensions include neck finish, outer neck diameter, inner bore diameter, bore depth, finish height, thread profile, ROPP finish, sealing surface, shoulder clearance, and closure head allowance.
Why is bore diameter important for bar-top stoppers?
Bore diameter controls how the stopper shank compresses inside the bottle neck. If the bore is too narrow, the stopper may be too tight. If it is too wide, the stopper may feel loose or fail to seal consistently.
When should buyers request closure samples?
Buyers should request closure samples before bulk production, especially for new bottle molds, premium stopper designs, export projects, automatic filling lines, custom decorative closures, ROPP caps, or unclear neck finish specifications.