What Is Screw Cap Compatibility Testing?
Screw cap compatibility testing checks whether a screw cap, liner, bottle neck finish, torque range, tamper-evident band, and capping-line setup work together as a complete closure system.
For spirits bottles, this test should happen before bulk cap production, custom decoration, liner approval, tooling, or export shipment. A cap may look correct on a sample bottle, but real performance depends on thread engagement, liner compression, application torque, removal torque, sealing surface accuracy, and filling-line conditions.
Before ordering custom screw caps, buyers should confirm bottle neck fit, liner contact, torque range, leakage resistance, and capping-line performance with real samples.
For spirits brands, distilleries, private label buyers, importers, distributors, bottlers, and packaging buyers, screw cap compatibility testing helps reduce packaging risk before products enter the market.
Who Needs Screw Cap Compatibility Testing?
Screw cap compatibility testing is useful for any buyer changing bottles, closures, liners, suppliers, or filling conditions.
It is especially important for spirits brands launching a new bottle, distilleries changing closure suppliers, private label buyers sourcing custom screw caps, importers concerned about leakage claims, bottlers validating capping-line settings, and distributors managing export packaging risk.
Testing is also recommended when a project involves custom aluminum screw caps, ROPP closures, high-ABV spirits, premium decoration, long-distance shipping, or a new bottle neck finish.
In short, if the closure has not been tested with the actual bottle and production method, the project still carries compatibility risk.
Why Testing Matters Before Production and Export
A screw cap is not only a decorative bottle top. It is part of a sealing system that protects the liquid, supports the brand experience, and helps the bottle survive filling, storage, transport, retail handling, and consumer opening.
If the screw cap does not match the bottle neck finish, the result may include leakage during shipment, loose caps after storage, over-tight closures, stripped threads, liner compression failure, tamper-evident band defects, distributor rejection, or delayed private label launches.
This matters because spirits packaging often faces more stress than simple local shelf packaging. Bottles may pass through sea freight, truck transport, warehouse storage, pallet pressure, temperature changes, and multiple handling points before reaching the final customer. For projects that include bottle development as well as closures, reviewing the complete custom glass packaging for spirits system early can reduce fit, decoration, and export packing risks.
ASTM International describes ASTM D2063/D2063M as a method for measuring torque retention properties of container and continuous-thread closure systems. This is relevant when packaging teams need to understand whether a threaded closure remains stable over time.
The practical lesson for buyers is simple: do not approve a screw cap only by appearance. Test the complete closure system before confirming bulk production.
What Must Be Compatible?
Successful screw cap compatibility testing reviews every important part of the cap-and-bottle system.
Bottle Neck Finish
The bottle neck finish controls how the screw cap engages, seals, and opens. Important dimensions include thread profile, neck diameter, sealing surface, neck height, bead position, and tolerance range.
A common sourcing mistake is assuming that cap diameter alone confirms compatibility. It does not. A 28 mm screw cap may not fit every 28 mm bottle if the thread structure, cap height, sealing surface, or neck tolerance is different.
For commercial projects, buyers can use a cap-neck compatibility review to check bottle drawings, neck finish details, closure type, sample photos, and physical bottle samples before bulk production.
Thread Engagement
Thread engagement determines whether the cap starts smoothly, tightens evenly, and stays secure after application.
Poor thread engagement can cause cross-threading, spinning, cap tilt, thread stripping, or unstable opening force. This is especially important for automatic capping lines, where small dimensional variations can create repeated production defects.
A good screw cap should start easily, rotate smoothly, reach the intended closing position, and maintain stable contact with the bottle neck after application.
Liner Contact
The liner is often the real sealing interface. The thread holds the cap in position, but the liner must compress against the bottle sealing surface to help prevent leakage.
A liner should be reviewed based on spirit type, alcohol percentage, filling temperature, contact time, aroma sensitivity, torque range, export market, and food-contact expectations.
For U.S. market projects, the FDA maintains an inventory of substances authorized in Title 21 of the Code of Federal Regulations for food-contact uses. This is one reason liner material selection should not be treated as a purely visual decision.
Cap Height and Tamper-Evident Band
Cap height affects appearance, thread coverage, tamper-evident function, and production performance.
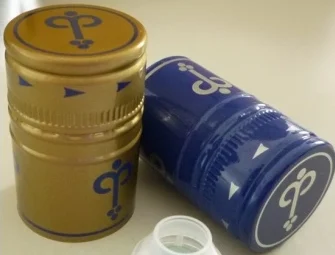
A short-skirt screw cap may suit compact bottles or RTD spirits packaging. A long-skirt aluminum screw cap may create a more premium appearance for whisky, vodka, gin, rum, tequila, or liqueur bottles.
If the closure includes a tamper-evident band, testing should confirm that the band sits in the correct position, holds during transport, and breaks cleanly during first opening.
Capping-Line Setup
A screw cap that works during manual sampling may fail on a production line.
Automatic or semi-automatic capping equipment introduces real operating variables, including application speed, chuck pressure, top pressure, roller setting, cap feeding, bottle stability, and production tolerance.
For ROPP closures, the capping-line setup is especially important because the closure is formed onto the bottle during application. In this case, compatibility depends not only on the cap and bottle, but also on machine settings.
Main Screw Cap Compatibility Tests
The best testing process combines visual review, dimensional confirmation, torque measurement, leakage review, and filling-line validation.
| Test Item | What It Checks | Buyer Risk Prevented |
|---|---|---|
| Visual fit test | Cap height, skirt position, straightness | Poor appearance or tilted cap |
| Thread engagement test | Internal thread and neck finish match | Cross-threading, spinning, stripped threads |
| Application torque test | Closing force during capping | Under-tightening or over-tightening |
| Removal torque test | Opening force after storage | Consumer complaints or loose caps |
| Liner compression test | Seal contact and liner recovery | Leakage and odor transfer risk |
| Leakage test | Seal integrity under stress | Export leakage claims |
| Tamper-evident band test | Band position and bridge break | Failed first-open evidence |
| Filling-line trial | Real machine performance | Production instability |
Visual Fit Test
The visual fit test checks whether the screw cap sits straight and aligns with the bottle neck.
Buyers should review whether the cap covers the neck correctly, whether the skirt height looks balanced, whether the cap tilts after tightening, and whether the tamper-evident band sits in the correct position.
This stage is simple but important. It can reveal major cap-neck mismatch issues before more detailed testing begins.
Thread Engagement Test
Thread engagement testing checks whether the cap starts smoothly, rotates correctly, and reaches the intended closing position.
The cap should not wobble, spin freely, cross-thread, or bottom out too early. If the cap feels unstable during hand application, it is unlikely to perform reliably during high-speed bottling.
Application Torque Test
Application torque measures the force used to apply the screw cap to the bottle.
If torque is too low, the liner may not compress enough to seal. If torque is too high, the cap may deform, threads may strip, or the closure may become difficult to open.
A stable torque range is especially important for bottlers using automatic or semi-automatic capping equipment. For a deeper technical reference, buyers can compare these factors with a dedicated screw cap torque guide before sample approval.
Removal Torque Test
Removal torque measures the force needed to open the cap.
This test affects both technical safety and consumer experience. A premium spirits bottle should feel secure, but it should not be frustrating to open.
Removal torque should be measured shortly after application and again after a defined rest period. This helps evaluate torque relaxation, liner recovery, and storage behavior.
Liner Compression Test
Liner compression testing confirms whether the liner creates consistent contact with the bottle sealing surface.
The liner should compress enough to seal, but not so much that it wrinkles, cracks, or loses recovery. For high-ABV spirits, buyers should also consider whether the liner is suitable for long-term alcohol contact and aroma protection.
Leakage Test
Leakage testing checks whether the screw cap and bottle remain sealed under expected storage and transport conditions.
A basic review may include upright storage, inverted storage, and side-position checks. A more complete review may include vibration, temperature variation, vacuum, or shipment simulation depending on order size and export risk.
For high-value spirits, leakage testing should not be delayed until after full production. It should be part of sample approval.
Tamper-Evident Band Test
Tamper-evident band testing confirms whether the band holds during handling and breaks properly at first opening.
The review should include bridge strength, band height, skirt retention, opening behavior, and whether the band interacts correctly with the neck bead or locking ring.
Filling-Line Trial
A filling-line trial is the most realistic stage of screw cap compatibility testing.
It confirms whether the selected closure works under actual production conditions. This is especially important for ROPP closures, high-speed capping lines, custom aluminum caps, decorated caps, and large export orders.
How to Know If a Screw Cap Passes or Fails
Buyers do not need to rely only on visual judgment. A practical compatibility review should define clear pass and fail signals.
| Test Area | Pass Signal | Fail Signal |
|---|---|---|
| Visual fit | Cap sits straight and skirt height is consistent | Tilted cap, uneven skirt, visible gap |
| Thread engagement | Smooth start and stable tightening | Cross-threading, spinning, rough rotation |
| Torque | Stable application and removal range | Too loose, too tight, unstable readings |
| Liner compression | Even sealing contact | Wrinkled liner, weak contact, compression set |
| Leakage | No liquid escape after stress checks | Wet carton, inverted leakage, cap loosening |
| Tamper band | Holds before opening and breaks cleanly | Early bridge break or difficult opening |
| Filling-line trial | Stable capping without repeated defects | Cap feeding issues, deformation, inconsistent seal |
This pass/fail table helps procurement teams, bottlers, and quality teams discuss closure performance using observable results instead of vague impressions.
Field Notes from Screw Cap Sample Testing
In real spirits packaging projects, many closure problems are not visible during the first manual fit check.
A cap may sit correctly by hand but show unstable torque on a semi-automatic or automatic capping line. A liner may seal during upright storage but fail after vibration, side-position testing, or long-distance shipment. A 28 mm screw cap may still mismatch a 28 mm bottle if the thread finish, sealing land, or skirt height is different.
ROPP closures create another layer of testing. The shell may look premium before application, but final performance depends on roller setting, top pressure, skirt formation, bridge break, and bottle neck accuracy.
For this reason, buyers should test the actual bottle, closure, liner, and capping method together. When possible, sample approval should include both hand checks and production-line trials before decoration or bulk order confirmation.
Standard Screw Cap vs ROPP Closure Testing
Many spirits buyers compare standard screw caps with ROPP closures. Both can be suitable, but they require different compatibility checks.
| Item | Standard Screw Cap | ROPP Closure |
|---|---|---|
| Thread source | Pre-formed internal thread | Formed onto bottle during capping |
| Key test focus | Thread fit, torque, liner compression | Roller forming, top pressure, torque, band |
| Machine dependency | Low to medium | High |
| Tamper evidence | Optional or integrated | Usually integrated |
| Main risk | Thread mismatch or weak seal | Poor forming or band failure |
For standard screw caps, the buyer should focus on thread match, cap height, liner compression, removal torque, and resealing performance.
For ROPP closures, the buyer should also test top pressure, thread roller setting, tuck roller performance, bridge break, pilfer band behavior, and production-line forming quality.
Buyers comparing the two options can review a detailed guide to ROPP closures vs screw caps before choosing a closure direction for sampling.
Common Screw Cap Problems and How to Diagnose Them
| Problem | Possible Cause | Recommended Test |
|---|---|---|
| Cap leaks in cartons | Low torque, weak liner compression, poor sealing land | Torque test + leakage test |
| Cap is hard to open | Over-torque, high thread friction, liner compression set | Removal torque test |
| Cap spins freely | Thread mismatch or stripped thread | Thread engagement test |
| Cap looks tilted | Neck finish tolerance issue or cap deformation | Visual fit + dimensional check |
| Tamper band breaks too early | Weak bridges or wrong band position | Tamper-evident band test |
| Leakage after sea freight | Torque relaxation, vibration, temperature change | Retention + shipment simulation |
| Liner wrinkles | Over-compression or wrong liner size | Liner compression review |
| Cap loosens after storage | Torque relaxation or poor thread engagement | Torque retention test |
This type of diagnostic table helps procurement teams connect visible packaging failures with measurable technical causes.
What Buyers Should Prepare Before Sample Testing
The quality of screw cap compatibility testing depends on the quality of project information.
Before requesting samples or a quotation, buyers should prepare:
- Bottle drawing or CAD file
- Physical bottle samples
- Bottle neck finish specification
- Existing closure sample, if available
- Target cap diameter and height
- Standard screw cap or ROPP closure preference
- Spirit type and alcohol percentage
- Filling temperature
- Manual, semi-automatic, or automatic capping method
- Capping machine model, if available
- Tamper-evident requirement
- Decoration method, such as printing, embossing, debossing, or color matching
- Export market
- Shipping method
- Estimated order quantity
- Target launch timeline
This information allows a closure supplier to recommend a more accurate cap structure, liner direction, torque review, and sample plan.
How to Evaluate a Screw Cap Supplier
A reliable screw cap supplier should not only sell by diameter. For spirits packaging, supplier capability should include technical review, sampling, material guidance, decoration support, and export production planning.
| Supplier Question | Why It Matters |
|---|---|
| Can you review bottle drawings and samples? | Confirms neck finish and cap fit before tooling or bulk production |
| Can you recommend liner options for spirits? | Reduces leakage, alcohol-contact, and aroma risk |
| Can you support torque and leakage review? | Helps prevent production defects and export claims |
| Can you provide pre-production samples? | Avoids approving caps only by photos or catalog dimensions |
| Can you support decoration after fit approval? | Protects both closure function and brand presentation |
| Can you support bulk export projects? | Helps align packaging, lead time, quality control, and shipment planning |
Kandacork Closures & Stoppers supports custom spirits bottle closures, screw caps for spirits bottles, ROPP closures, neck-fit review, branding, sampling, and bulk export projects.
Recommended Testing Workflow Before Bulk Order
A practical screw cap compatibility testing workflow should include:
- Confirm bottle type and neck finish.
- Share bottle drawing and physical samples.
- Select standard screw cap or ROPP closure direction.
- Choose cap material, height, skirt style, and decoration method.
- Review liner options based on spirit type and ABV.
- Request sample caps and check visual fit.
- Measure torque, liner compression, and leakage performance.
- Run a filling-line trial using real equipment.
- Approve the final technical specification before bulk production.
This process helps buyers avoid a common packaging mistake: approving the cap visually before confirming production performance.
FAQ
What is screw cap compatibility testing?
Screw cap compatibility testing checks whether the screw cap, liner, bottle neck finish, torque range, tamper-evident band, and capping process work together as a complete closure system.
Is cap diameter enough to confirm compatibility?
No. Cap diameter is only one part of the specification. Buyers must also check thread profile, cap height, liner contact, sealing surface, tamper-evident band position, and capping equipment.
Why do screw caps leak?
Screw caps may leak because of low application torque, poor liner compression, bottle neck mismatch, damaged threads, cap deformation, unsuitable liner material, or torque relaxation during storage and shipment.
Why are application torque and removal torque both important?
Application torque shows whether the cap can be applied with enough force to seal. Removal torque shows whether the cap can still be opened properly after storage. Both matter because the closure must seal securely but remain practical for consumers.
What should buyers send for screw cap sample testing?
Buyers should send bottle drawings, physical bottle samples, bottle neck finish details, spirit type, alcohol percentage, filling conditions, capping method, decoration requirements, export market, and estimated order quantity.