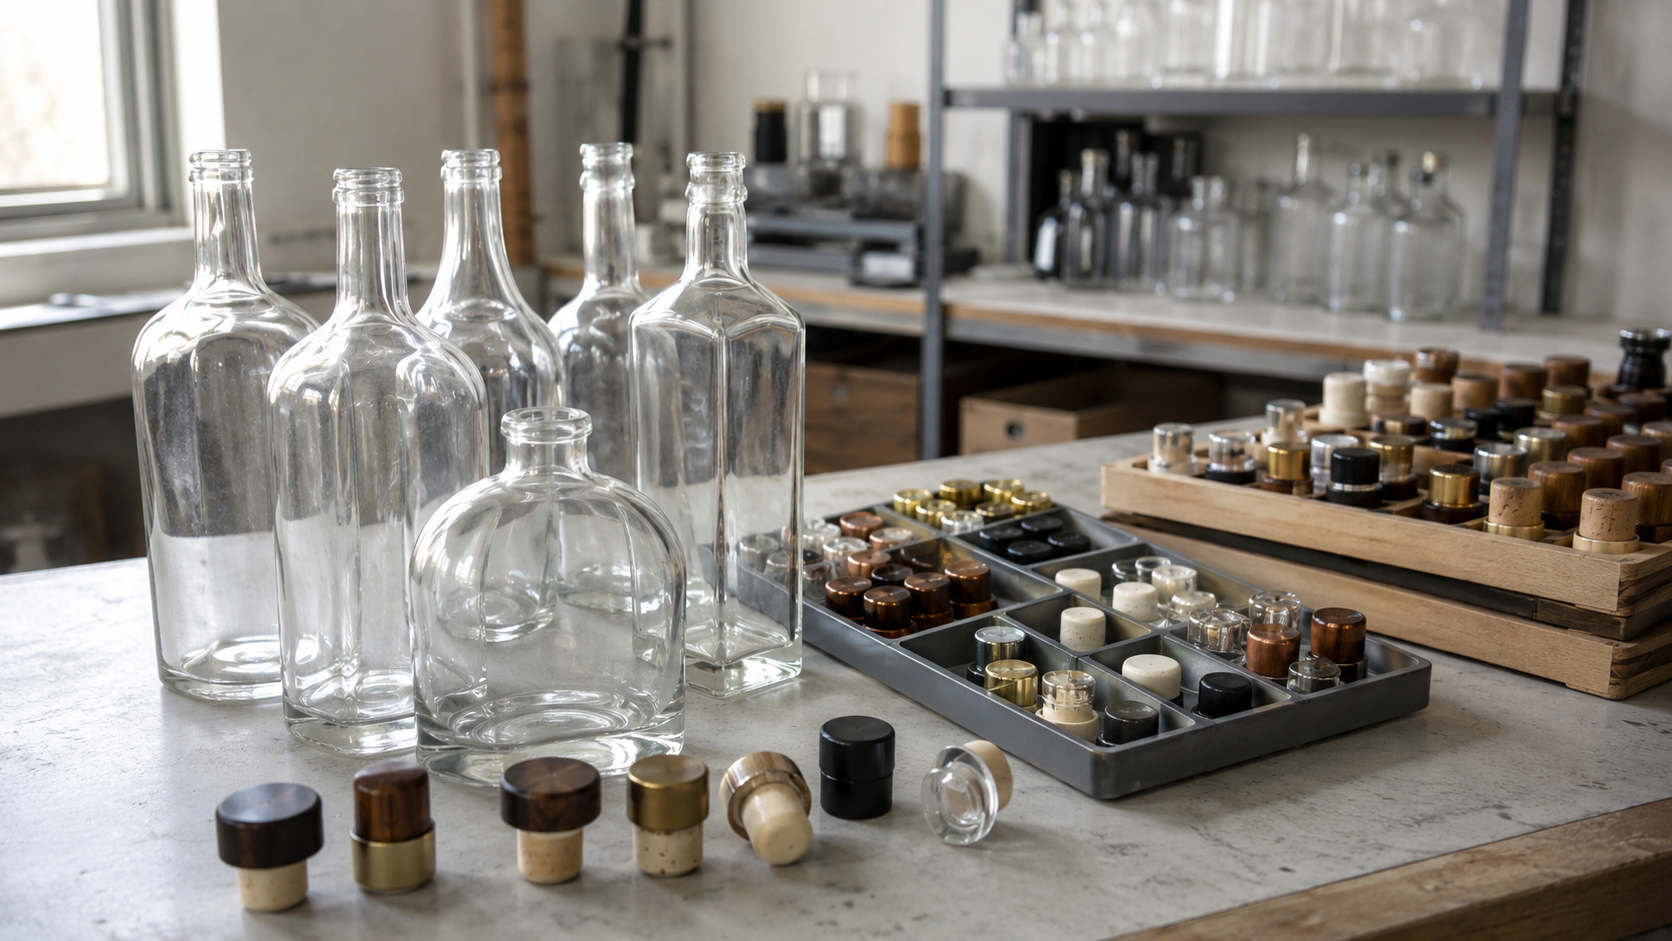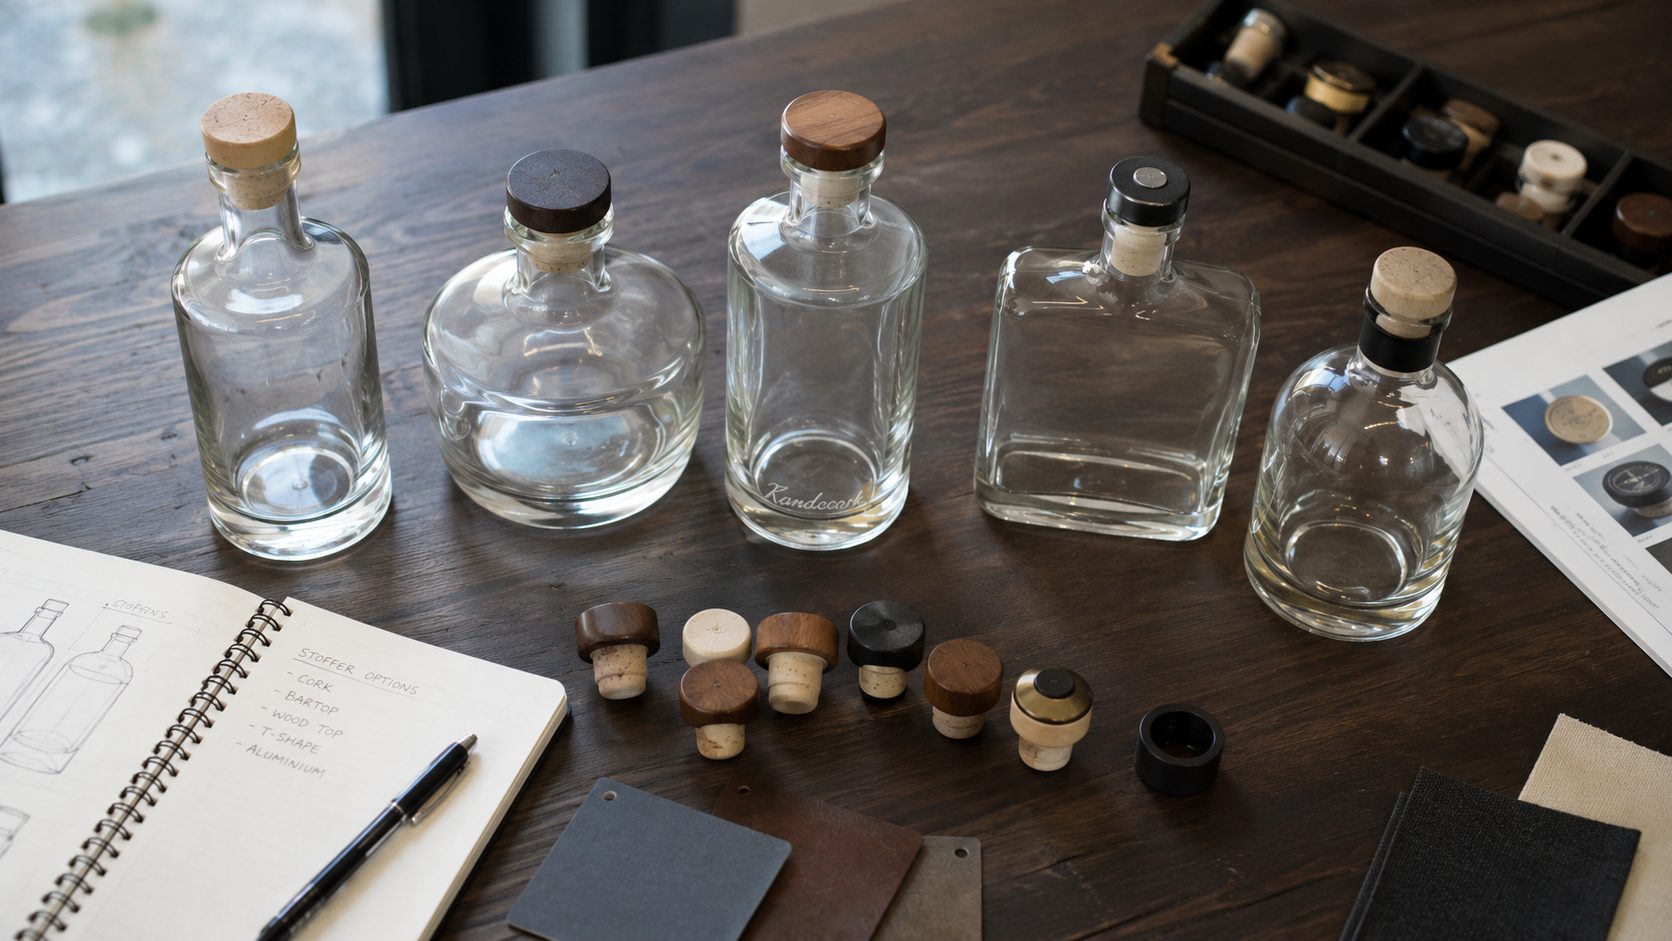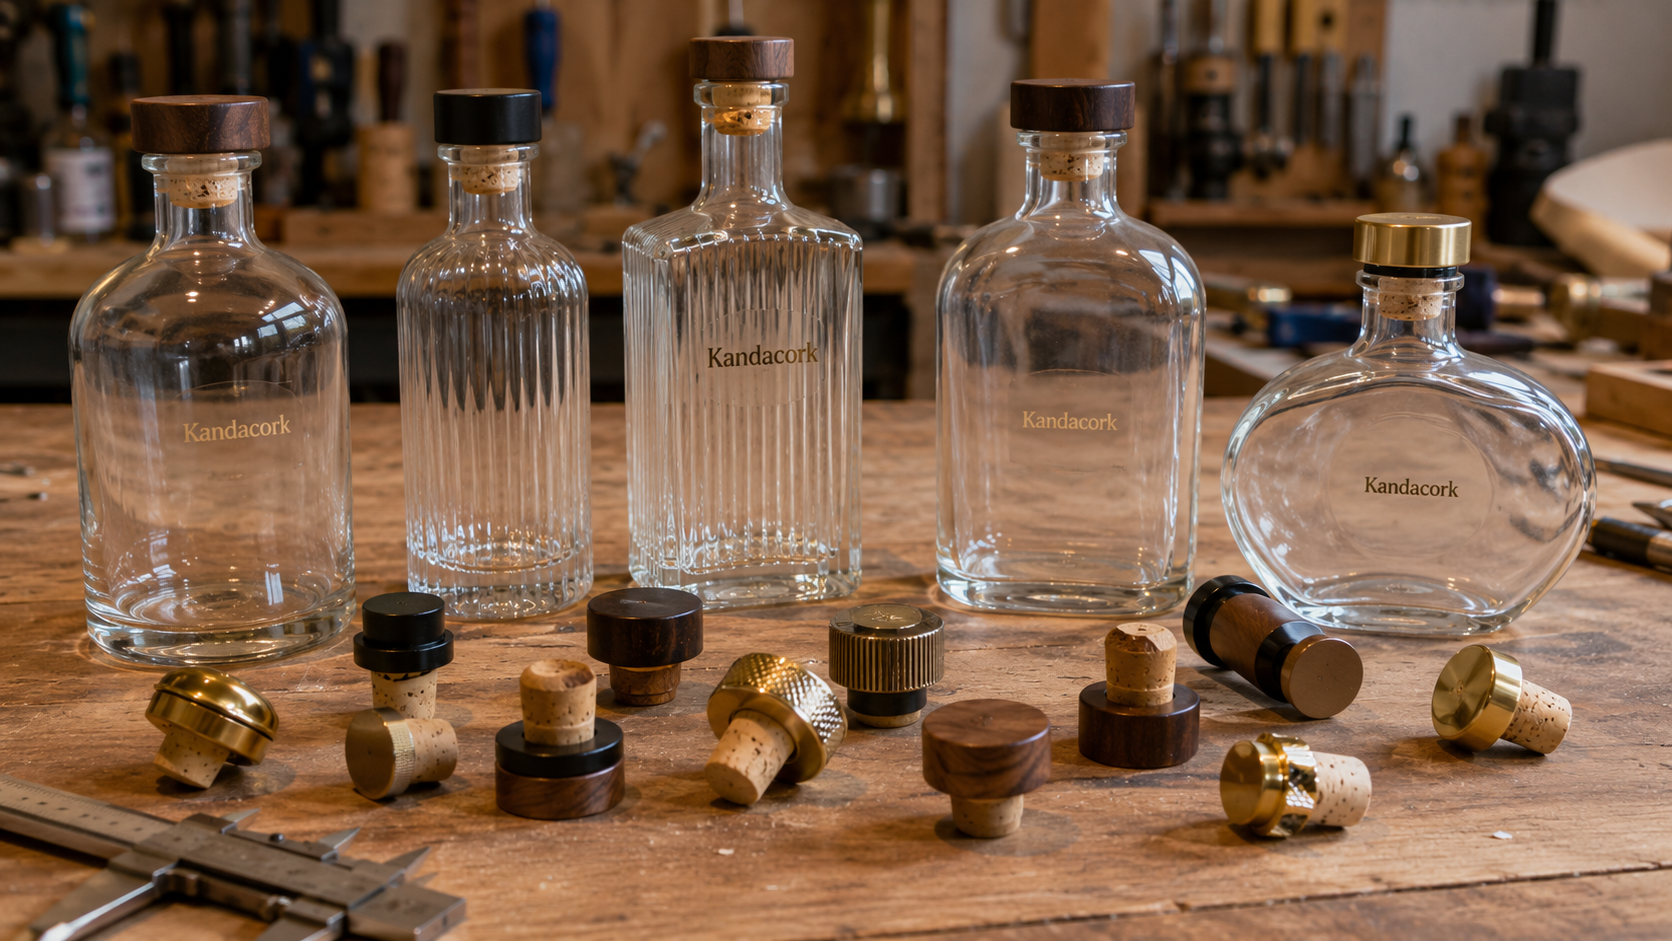
Bar-top stopper rework before shipment can delay spirits packaging projects, increase sorting costs, disrupt bottling schedules, and weaken finished bottle presentation. For spirits brands, distilleries, private label buyers, importers, distributors, bottlers, and packaging buyers, the issue usually points to a gap in bottle fit confirmation, sample approval, material control, decoration standards, inspection criteria, or export packing.
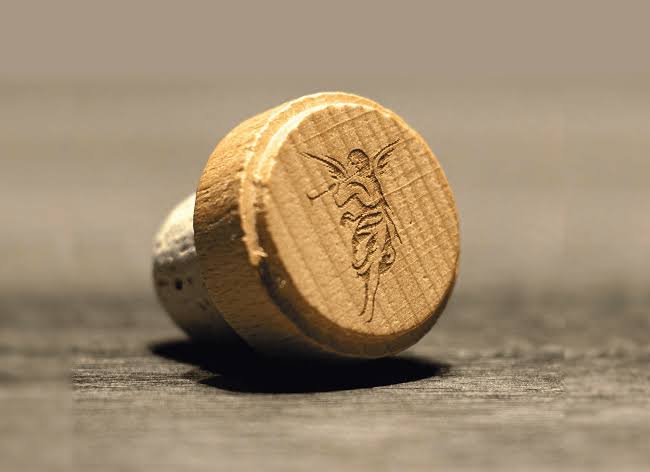
A bar-top stopper must fit the bottle neck, seal securely, open smoothly, support premium shelf appeal, and survive handling during international transport. If the stopper is loose, too tight, scratched, misprinted, tilted, mixed, or poorly packed, the order may require rework before shipment approval.
The best way to reduce bar-top stopper rework is to prevent defects before mass production. Kandacork Closures helps spirits packaging buyers reduce these risks through bottle-to-stopper matching, material selection, custom decoration, sample approval, production inspection, and export-ready packing for custom wooden bar-top stoppers and other spirits closure projects.
Quick Answer: How Do You Reduce Bar-Top Stopper Rework Before Shipment?
To reduce bar-top stopper rework before shipment, confirm bottle neck dimensions, test physical samples, approve a golden sample, define critical, major, and minor defects, inspect shank diameter and logo quality, test stopper fit with real bottles, and verify export packing before shipment approval.
The most important controls are:
- Measure the bottle mouth inner diameter.
- Confirm the neck tolerance range.
- Review the internal neck profile.
- Match the shank diameter to the bottle neck.
- Test stopper insertion and pull-out feel.
- Approve material, color, logo, and surface finish.
- Define acceptable and unacceptable defects.
- Inspect dimensions, appearance, assembly, and packing.
- Request inspection photos and reports before shipment.
When these controls are handled early, buyers can reduce sorting, replacement, repacking, delayed delivery, and bottling-line disruption.
What Is Bar-Top Stopper Rework?
Bar-top stopper rework means correcting product defects or inconsistencies before an order can be shipped or accepted. In a spirits closure project, rework may include sorting, cleaning, replacing, repacking, relabeling, reassembling, or remaking part of the order.
Common examples include scratched wooden tops, logo misprints, mixed sizes, mixed SKUs, tilted caps, loose shanks, glue overflow, wrong color, unstable fit, damaged cartons, or incorrect carton marks.
Some rework is minor and can be completed quickly. Other rework can delay shipment booking, filling schedules, distributor delivery, or retail launch plans. For private label spirits projects and export orders, closure problems can be costly because packaging components often need to arrive within a fixed production window.
Why Rework Matters for Spirits Buyers
A stopper defect can affect more than appearance. It may influence filling efficiency, finished bottle consistency, consumer experience, and incoming inspection at the destination warehouse.
For example, a premium rum brand may choose a wood-top stopper because it gives the bottle a warmer and more traditional look. If the wooden tops arrive with visible scratches or uneven stain color, the final package may look inconsistent on shelf. A whiskey bottler may choose a synthetic shank for dimensional stability, but if the shank diameter is not matched to the bottle neck, the stopper may feel loose during handling or too tight for consumers to remove.
Bar-top stopper rework creates several business risks:
- Shipment delay due to sorting or replacement
- Higher labor cost for inspection and rework
- Missed bottling windows
- Distributor delivery delays
- Incoming inspection rejection
- Mixed SKU problems during filling
- Premium brand image damage
- Extra communication between buyer, supplier, freight forwarder, and bottler
Reducing rework protects both packaging quality and commercial timelines.
Fit Check: Bottle Neck and Shank Measurements
Fit-related issues are among the most common causes of stopper rework. A bar-top stopper must compress properly inside the bottle mouth. If the shank is too small, the stopper may feel loose, rotate easily, or pop up during handling. If the shank is too large, insertion can become difficult and bottling-line efficiency may suffer.
As a common starting point, many bar-top stopper projects use a shank diameter about 1 mm larger than the bottle mouth inner diameter to create a secure friction fit. However, this should not be treated as a fixed rule. Final sizing should consider neck tolerance, internal neck profile, shank material, compression behavior, insertion depth, pull-out feel, and real bottle testing.
Buyers should not rely only on bottle capacity, such as 700 ml or 750 ml. The key information is the bottle mouth inner diameter, neck profile, tolerance range, shank diameter, shank length, and target insertion depth. For buyers working with uncertain bottle-neck data, a dedicated glass bottle neck closure matching guide can help turn drawings, samples, and measurements into a clearer closure specification.
| Check Item | Why It Matters | Rework Risk If Ignored |
|---|---|---|
| Bottle mouth inner diameter | Determines starting shank size | Loose fit or over-tight insertion |
| Neck tolerance range | Shows possible bottle variation | Inconsistent seating height |
| Internal neck profile | Identifies taper, restriction, or pinch points | Stopper pop-up or unstable fit |
| Shank diameter | Controls sealing feel and hold | Loose stopper or hard insertion |
| Shank length | Affects insertion depth and grip | Poor stability or uneven appearance |
| Total stopper height | Affects finished bottle presentation | Inconsistent shelf appearance |
| Pull-out feel | Affects consumer experience | Too loose or too difficult to open |
| Bottle sample test | Confirms real-world compatibility | Bulk shipment rejection |
For custom spirits packaging projects, Kandacork Closures recommends testing stopper samples with actual bottles whenever possible. Bottle drawings are important, but physical bottle samples help confirm real fit, especially when glass tolerance varies across molds, production batches, or bottle suppliers.
Neck Profile Measurement Before Sampling
A simple mouth measurement is helpful, but it may not show the full fit risk. Some bottles have internal taper, uneven wall thickness, or a narrow point below the opening. These details can affect stopper insertion and seating height.
| Measurement Step | Purpose | Buyer Benefit |
|---|---|---|
| Measure mouth inner diameter | Confirm starting shank size | Avoid loose or over-tight fit |
| Check neck depth | Confirm the insertion zone | Avoid unstable seating height |
| Review internal neck profile | Identify taper or pinch points | Reduce stopper pop-up risk |
| Test several bottle samples | Confirm bottle tolerance variation | Avoid batch-level fit issues |
| Record insertion feel | Check bottling-line practicality | Reduce production slowdown |
| Record pull-out feel | Confirm user experience | Reduce complaints after bottling |
For high-volume spirits projects, buyers should provide several bottle samples if available. This helps the supplier evaluate variation instead of designing the stopper around only one ideal bottle.
Golden Sample Approval Checklist
A golden sample is the approved physical reference for mass production. It should represent the final quality standard, not just the general design direction.
A strong golden sample should confirm:
- Stopper size
- Top shape
- Shank material
- Cap material
- Surface finish
- Logo method
- Logo position
- Color standard
- Insertion feel
- Pull-out feel
- Seating height
- Packing method
For custom logo stoppers, the golden sample should also confirm artwork file accuracy, logo size, logo placement, embossing or debossing depth, printing density, foil tone, coating texture, and acceptable color variation. If the closure top or sidewall needs branded grip details, texture, or logo placement, early review of closure sidewall branding and grip-area design can help reduce decoration-related rework. During production and pre-shipment inspection, the order can be compared against the golden sample to reduce subjective disagreement.
Material Selection and Rework Risk
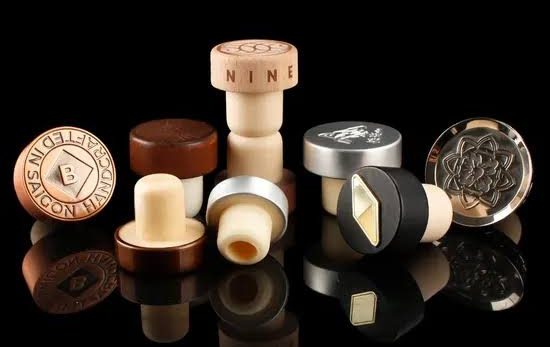
The right bar-top stopper material depends on brand positioning, bottle design, target market, production process, budget, and quality expectations. The best option is the material system that balances appearance, dimensional consistency, production stability, and shipment protection.
| Material Option | Advantages | Rework Risk to Control |
|---|---|---|
| Wooden top | Premium, natural, suitable for whiskey, rum, brandy, tequila | Grain variation, color difference, scratches |
| Plastic top | Cost-effective, stable color, flexible molding | Burrs, molding marks, lower premium feel |
| Aluminum top | Modern, clean, premium metallic look | Scratches, dents, plating marks |
| Metal top | Strong shelf impact and weight | Surface damage, plating consistency |
| Glass top | Distinctive and high-end | Breakage, weight, transport protection |
| Natural cork shank | Traditional and natural image | Diameter variation, cork dust, odor |
| Micro-agglomerated cork shank | More consistent than natural cork | Compression and surface treatment control |
| Synthetic shank | Stable dimensions and repeatability | Material compatibility and insertion feel |
Commercial buyers should evaluate unit price together with rework probability, inspection difficulty, lead time, and final bottle presentation.
Common Bar-Top Stopper Rework Problems and How to Prevent Them
Most rework problems come from unclear specifications, weak sample approval, unstable production control, or insufficient packing review. The table below connects typical defects with likely causes, buyer risks, and prevention methods.
| Defect | Likely Cause | Buyer Risk | Prevention Method |
|---|---|---|---|
| Loose stopper fit | Shank too small or bottle tolerance ignored | Poor user experience, unstable closure | Confirm bottle inner diameter and test samples |
| Over-tight insertion | Shank too large or material too rigid | Bottling slowdown, bottle damage risk | Adjust shank size and compression |
| Stopper pop-up | Poor fit or insufficient insertion depth | Shipment and shelf presentation issue | Test insertion depth and pull-out feel |
| Tilted top | Poor assembly or drilling control | Premium appearance failure | Use in-process assembly checks |
| Uneven seating height | Shank length or neck variation | Inconsistent finished bottle look | Compare with golden sample |
| Logo off-center | Weak fixture or artwork control | Brand image problem | Approve artwork and first-piece sample |
| Color mismatch | No physical color reference | Visual inconsistency | Use Pantone or approved color sample |
| Scratched cap | Poor handling or packing | Sorting, rework, claim risk | Use protective packing and surface checks |
| Glue overflow | Excess adhesive or poor assembly | Cosmetic defect | Improve assembly process control |
| Mixed specifications | Weak batch separation | Bottling errors and shipment delay | Verify SKU labels and carton marks |
This table helps procurement, packaging development, and QC teams turn vague quality concerns into specific supplier control points.
In-Process QC and Pre-Shipment Inspection Checklist
Pre-shipment inspection should not be the first time defects are discovered. In-process quality control helps identify problems while they are still easier to correct.
Incoming Material Inspection
Incoming inspection should check wood blanks, cork material, synthetic shanks, metal parts, plastic components, coatings, adhesives, and printing materials. Raw material instability often leads to finished product inconsistency.
Inspection may include color, odor, moisture condition, surface defects, diameter, hardness, batch information, and visible contamination.
First-Piece Approval
Before full production begins, the first finished pieces should be checked against the drawing and golden sample. This step is especially important for custom logo stoppers, colored tops, special finishes, and new bottle projects.
First-piece approval should confirm size, assembly, color, logo position, surface finish, fit with bottle, and packing method. If the first pieces are wrong, production should stop before the defect spreads across the batch.
Dimensional and Functional Inspection
Critical dimensions should be checked during production and before shipment. For bar-top stoppers, these usually include shank diameter, shank length, top diameter, top height, total height, drilling depth, head flatness, shank straightness, and seating height.
Functional inspection should be performed with actual bottles or approved bottle samples whenever possible. Inspectors should check insertion feel, pull-out resistance, seating height, stopper straightness, repeated opening feel, and overall bottle compatibility.
Appearance Inspection
Appearance inspection should check scratches, dents, dust, coating marks, color spots, logo defects, burrs, cracks, deformation, plating issues, printing blur, and surface contamination.
For premium spirits closures, visible defects on the top surface should be controlled carefully because the stopper contributes directly to shelf appeal.
Packing Inspection
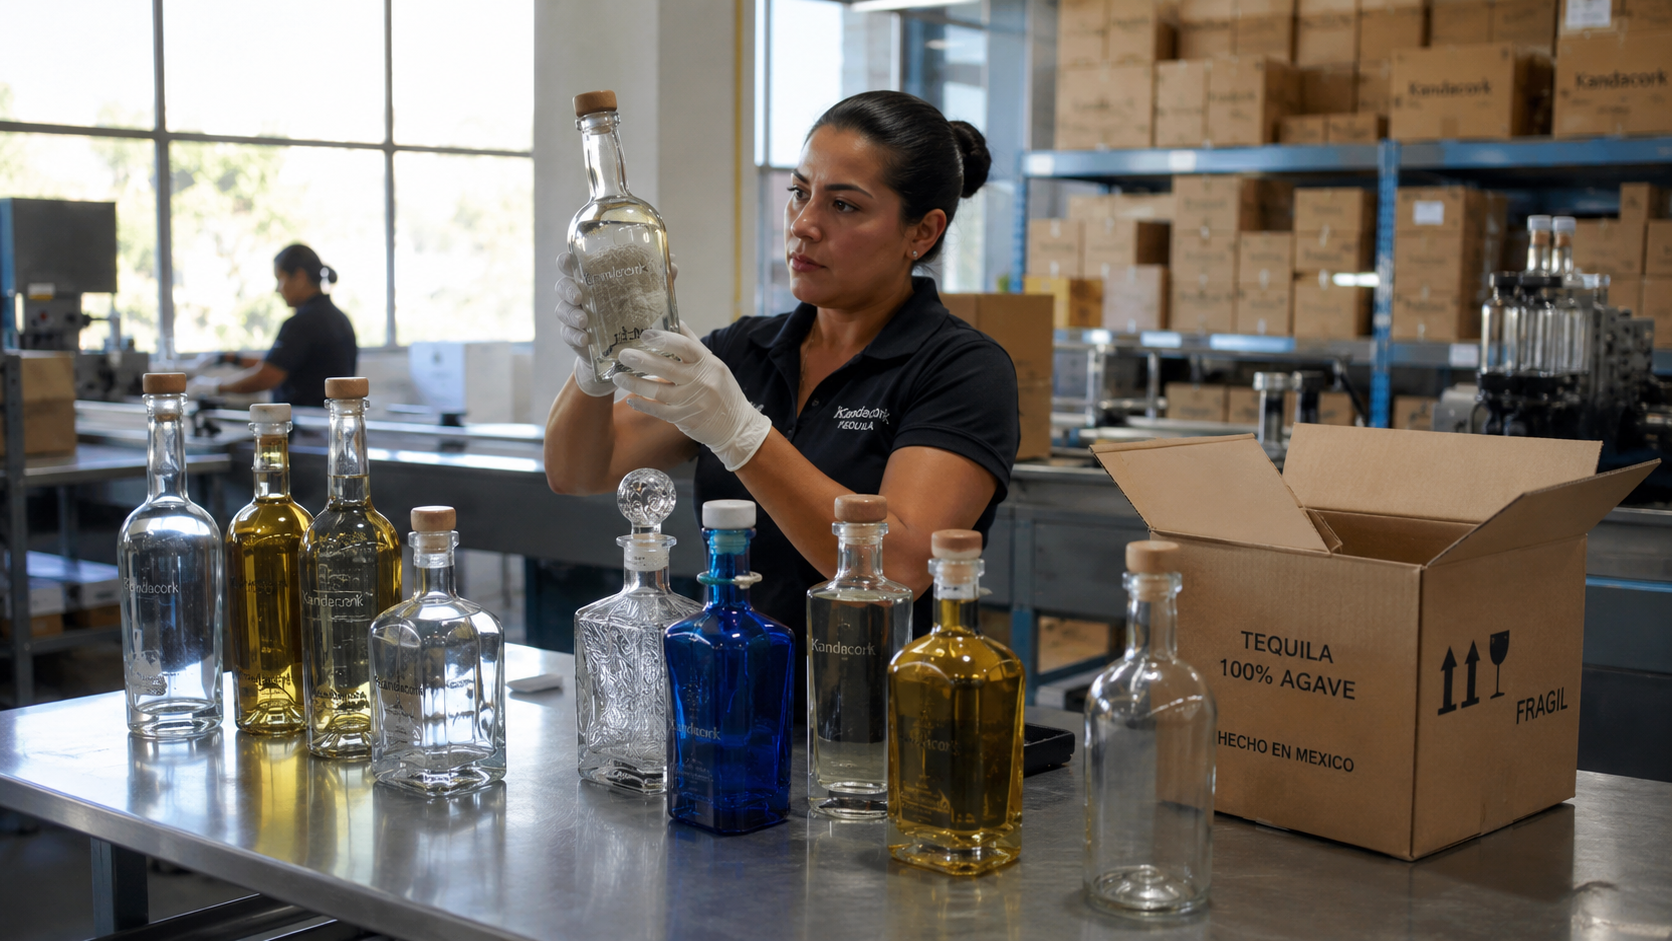
Packing should be reviewed before shipment approval, especially for premium wooden, painted, metal, plated, or glass-top closures. Buyers should check inner bags, dividers, carton strength, master cartons, labels, export marks, pallet wrapping, moisture protection, and mixed-SKU prevention.
For export projects, ASTM D4169 and ISTA test procedures are useful reference entities for distribution package testing and transport simulation. Buyers do not always need full laboratory testing for every order, but these standards help frame why carton strength, compression resistance, handling protection, and pallet security matter. Buyers can also compare these checks with an export-ready closure supplier process when preparing shipment approval requirements.
Documentation Review
Before shipment approval, buyers should request inspection photos, packing photos, batch numbers, packing list, sample approval records, material information, and rework records if issues were found.
Defect Classification and AQL Sampling
Clear defect classification reduces disputes between buyer and supplier. It also helps determine whether the shipment can proceed, requires sorting, or needs replacement.
| Defect Type | Example | Suggested Classification |
|---|---|---|
| Wrong shank size | Stopper does not fit approved bottle | Critical or Major |
| Strong odor | May affect packaging confidence | Critical |
| Mixed SKU | Wrong sizes or colors in same carton | Critical or Major |
| Loose bonding | Shank separates from top | Major |
| Stopper pop-up | Stopper does not stay seated | Major |
| Logo off-center | Visible branding defect | Major |
| Wrong color | Does not match approved sample | Major |
| Visible top scratch | Affects premium appearance | Major |
| Slight hidden scratch | Not visible after bottling | Minor |
| Minor color variation | Within approved range | Minor |
Critical defects usually affect safety, usability, material suitability, or shipment identity. Major defects affect function, brand appearance, or bottling performance. Minor defects are small variations that do not affect normal use or visible presentation.
For larger orders, buyers may use an AQL-based sampling plan to inspect bar-top stoppers before shipment. AQL does not mean defects are desired. It provides a structured method for selecting sample size and judging whether a batch should be accepted, rejected, sorted, or reworked.
International quality frameworks such as ISO 2859-1 acceptance sampling and ANSI/ASQ Z1.4 are commonly referenced for acceptance sampling by attributes. For premium launches, first-time supplier orders, urgent shipments, or high-value decoration projects, buyers may request stricter inspection, additional sampling, or 100% sorting for key defects.
What Should Buyers Do If Defects Are Found Before Shipment?
If defects are found before shipment, buyers should avoid approving cargo release until the problem is classified, the affected quantity is confirmed, and corrective action is documented.
| Step | Buyer Action | Purpose |
|---|---|---|
| Hold shipment approval | Pause release until the issue is reviewed | Prevent defective goods from leaving the factory |
| Classify defects | Separate critical, major, and minor issues | Decide whether shipment can proceed |
| Confirm affected scope | Check cartons, batches, colors, and SKUs | Identify isolated vs batch-wide problems |
| Choose corrective action | Sort, rework, replace, remake, or re-inspect | Control cost, timing, and quality risk |
| Request evidence | Ask for photos, rework records, and updated report | Confirm the issue was corrected |
| Approve shipment release | Release only after review is complete | Protect the bottling schedule and brand quality |
For urgent projects, buyers may accept minor defects within agreed limits, but critical fit, mixed SKU, unsafe material, strong odor, or major branding defects should be resolved before shipment.
Supplier Capability Scorecard
A capable bar-top stopper supplier should do more than provide a product catalog. The supplier should help prevent rework through technical review, sampling, quality control, documentation, and export packing support. Buyers can use a bar-top closure project checklist to prepare key details before comparing supplier capability.
| Evaluation Area | Good Supplier Evidence |
|---|---|
| Fit support | Reviews bottle drawing, neck tolerance, and physical bottles |
| Neck profile review | Checks taper, insertion depth, and potential pinch points |
| Sampling | Provides golden sample before bulk production |
| Material guidance | Recommends cap and shank materials by project need |
| Decoration control | Confirms artwork, logo position, color, and finish |
| Dimensional QC | Checks shank diameter, total height, and tolerance |
| Functional QC | Tests insertion, pull-out feel, and seating height |
| Batch control | Separates SKUs, colors, and production batches |
| Packing | Uses export cartons, dividers, labels, and pallet protection |
| Reporting | Provides photos, inspection summary, and batch records |
| Rework process | Defines sorting, replacement, and re-inspection steps |
This scorecard helps buyers compare suppliers by capability, not only by price. A low unit price may become expensive if the supplier cannot control fit, appearance, packing, and shipment consistency.
Buyer-Side Incoming Inspection After Arrival
Even after pre-shipment inspection, importers, distributors, and bottlers should perform a short incoming inspection before moving closures to the filling line. This step helps catch transport damage, mixed cartons, or batch inconsistency before bottling begins.
Buyer-side incoming inspection should include:
- Carton count check
- SKU and carton label verification
- Batch number comparison
- Random fit test with production bottles
- Surface damage check
- Logo consistency check
- Color and finish review
- Packing damage review
- Report of discrepancies before bottling
This does not replace supplier-side quality control. It provides an additional safeguard before closures enter production.
Buyer RFQ Checklist
To receive a more accurate quotation and reduce future rework, buyers should prepare the following information before requesting samples or bulk pricing:
- Bottle drawing
- Bottle mouth inner diameter
- Neck tolerance range
- Bottle sample if available
- Stopper style reference
- Top material preference
- Shank material preference
- Target color or finish
- Logo artwork file
- Decoration method preference
- Target quantity
- Destination market
- Packing requirements
- Required documents
- Timeline
A product photo can help communicate style, but it is not enough for accurate production. Bottle drawings, neck measurements, artwork files, color references, material preferences, and physical samples help the supplier recommend the right closure structure and reduce late-stage adjustments.
For buyers managing a full packaging system, broader coordination between bottle structure, closure fit, decoration, and export preparation can also be reviewed through integrated spirits glass packaging support.
Request a Bar-Top Stopper Sample Review
Before approving bulk production, buyers can reduce risk by reviewing bottle fit, material selection, decoration details, and packing requirements with the supplier.
To request a more accurate sample review or quotation from Kandacork Closures, prepare:
- Bottle drawing or technical neck information
- Bottle mouth inner diameter
- Neck tolerance range if available
- Physical bottle samples if possible
- Preferred stopper style and material
- Logo artwork file
- Target color, finish, or decoration method
- Estimated order quantity
- Destination market
- Shipment timeline
- Required inspection or documentation needs
Kandacork Closures can help review stopper fit, shank options, custom decoration, golden sample requirements, pre-shipment inspection points, and export packing before bulk production. Buyers can submit project details through the Kandacork Closures sample review and quotation page.
Recommended Visuals for the Page
To improve readability and buyer understanding, the final page should include four core technical visuals.
| Visual | Purpose | Suggested Alt Text |
|---|---|---|
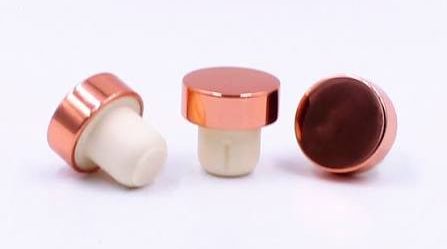
| Bar-top stopper structure | Explain cap and shank | bar-top stopper cap and shank structure |
| Bottle neck measurement | Support fit check | bottle neck inner diameter for bar-top stopper sizing |
| Correct vs loose vs tight fit | Explain rework causes | bar-top stopper fit inspection before shipment |
| Rework decision tree | Show corrective action process | bar-top stopper rework decision process before shipment |
These visuals can make the article easier to scan and more useful for procurement, QC, and packaging development teams.
How Kandacork Closures Helps Reduce Rework
Kandacork Closures helps spirits packaging buyers reduce bar-top stopper rework by connecting bottle fit review, custom closure development, production inspection, and export packing into one controlled sourcing process.
For bottle-to-stopper matching, Kandacork Closures can review bottle neck data, internal neck profile, stopper dimensions, shank material, and expected insertion performance. This helps reduce fit-related issues before production begins.
For custom branding, Kandacork Closures supports logo review, decoration method selection, color matching, surface finish confirmation, and golden sample approval. This helps buyers avoid late-stage issues such as off-center logos, color mismatch, weak embossing, or unsuitable coating.
For shipment readiness, Kandacork Closures can support dimensional checks, appearance standards, functional fit tests, batch traceability, carton protection, labeling, pallet security, mixed-SKU prevention, and rework evidence review when needed.
FAQ
What causes most bar-top stopper rework before shipment?
Most bar-top stopper rework is caused by bottle neck and shank mismatch, unclear specifications, decoration defects, material variation, weak assembly control, mixed batches, or poor export packing. These issues can usually be reduced through better sampling, golden sample approval, dimensional checks, fit testing, and pre-shipment inspection.
How can I check if a bar-top stopper fits my bottle?
Check the bottle mouth inner diameter, neck tolerance range, internal neck profile, shank diameter, insertion depth, seating height, and pull-out feel. The most reliable method is to test physical stopper samples with actual bottles from the same production batch or mold range.
Is the stopper shank always 1 mm larger than the bottle opening?
A shank diameter about 1 mm larger than the bottle mouth inner diameter is a common starting point for many bar-top stopper projects, but it is not a universal rule. Final sizing should be confirmed by bottle tolerance, shank material, compression behavior, insertion depth, pull-out feel, and physical sample testing.
What should be included in a stopper golden sample?
A stopper golden sample should confirm size, top shape, shank material, cap material, color, logo method, logo position, surface finish, insertion feel, pull-out feel, seating height, and packing method.
What defects should be checked before shipment?
Before shipment, buyers should check dimensions, appearance, logo quality, color, surface finish, assembly strength, stopper fit, seating height, batch consistency, packing, carton marks, and shipment documents.
When should buyers request 100% inspection?
Buyers should consider 100% inspection when the order is for a premium launch, first-time supplier production, urgent shipment, high-value custom decoration, previous quality failure, or when defects could stop the bottling line.
What documents should a closure supplier provide before shipment?
Useful documents include inspection reports, packing lists, batch numbers, production photos, packing photos, sample approval records, material information, and rework records if defects were found during inspection.