Quick Answer: What Is Cap and Neck Compatibility for Private Mold Bottles?
Cap and neck compatibility for private mold bottles means the bottle neck finish, inner bore, thread profile, sealing surface, and closure structure are engineered to work together before sampling, filling, or bulk production.
For private mold spirits bottles, buyers should confirm the closure type, neck dimensions, bore tolerance, liner or stopper shank fit, torque, leakage risk, tamper-evident function, and filling-line method before approving the bottle mold.
This matters because a custom spirits bottle may not follow a standard stock bottle finish. A bottle can look premium but still fail if the cap, stopper, ROPP closure, or non-refillable closure does not seal, fit, open, or apply correctly.
Kandacork Closures & Stoppers helps spirits brands, distilleries, private label buyers, importers, distributors, bottlers, and packaging buyers review bottle drawings, neck finish details, closure options, samples, testing requirements, decoration, and export packing before quotation or bulk approval.
Why Closure Fit Matters Before Private Mold Approval
Private mold bottles help spirits brands create a strong shelf identity. A whisky brand may want a heavy glass base and short neck. A tequila brand may choose a wide shoulder and decorative bar-top stopper. A vodka or gin brand may prefer a slim bottle with a clean aluminum closure.
These design choices support branding, but they also create technical risk. If the bottle mold is approved before the closure is selected, the neck finish may not match the desired cap or stopper. Correcting this later can require new samples, closure changes, filling-line adjustments, or even bottle mold correction.
Closure fit affects:
- sealing performance;
- leakage control;
- opening and reclosing feel;
- pull-out force;
- application and removal torque;
- tamper evidence;
- filling-line efficiency;
- export transport safety;
- consumer experience.
For U.S.-bound distilled spirits packaging, buyers should review the Alcohol and Tobacco Tax and Trade Bureau’s requirements related to tamper-evident closures for distilled spirits. For complete bottle-and-closure planning, packaging buyers can also compare neck finish options through this whiskey bottle neck finish guide from Kandacork Glass.
In private mold spirits bottle projects, Kandacork usually recommends reviewing the closure direction before the bottle neck ring is finalized. This helps buyers avoid approving a premium bottle shape first and discovering later that the preferred stopper, screw cap, ROPP cap, or non-refillable closure cannot be applied reliably.
The best time to check cap and neck compatibility for private mold bottles is before the bottle mold is finalized.
Key Bottle Neck Dimensions Buyers Should Check
Closure compatibility is not based on diameter alone. Buyers should review the full neck finish, especially when working with private mold spirits bottles.
| Neck Dimension | What It Means | Why It Matters |
|---|---|---|
| T Dimension | Outside diameter across the thread or finish | Helps match screw caps, CT caps, and some ROPP closures |
| E Dimension | Outside diameter of the neck below the thread area | Affects cap wall clearance, capsule fit, shrink sleeve fit, and tamper-band position |
| I Dimension / Inner Bore | Inside opening of the bottle neck | Critical for bar-top stoppers, synthetic shanks, cork shanks, inserts, pourers, and non-refillable closures |
| H Dimension | Height of the neck finish | Affects cap coverage, liner contact, ROPP forming, and visual fit |
| S Dimension / Thread Start | Thread engagement area | Affects screw cap application, torque, and thread stability |
| Sealing Land | Top sealing surface of the bottle mouth | Determines liner compression and leakage control |
For private mold bottles, these dimensions should be checked on both the technical drawing and real glass samples. Glass production tolerances can make the actual bottle slightly different from the drawing.
If you already have a bottle drawing or sample, Kandacork can support a cap and neck compatibility review before sample confirmation.
Closure Compatibility Matrix for Private Mold Spirits Bottles
Different closures require different neck structures. This matrix helps buyers compare options before requesting samples or quotations.
| Closure Type | Key Neck Requirement | Main Compatibility Test | Common Failure Risk |
|---|---|---|---|
| Bar-top stopper | Inner bore, insertion depth, shank compression | Pull-out force, leakage test, resealing test | Loose stopper, wobble, leakage |
| Synthetic stopper | Bore tolerance, shank hardness, molded size | Compression test, insertion test, storage test | Too tight, too loose, poor recovery |
| CT screw cap | Thread finish, sealing land, cap height | Application torque, removal torque, liner contact | Leakage, cross-threading, weak seal |
| ROPP cap | ROPP neck finish, pilfer band area, cap skirt | Cap forming, bridge break, opening torque | Spinning cap, broken band, high torque |
| Non-refillable closure | Bore shape, insert seat, valve position | Pour test, insert retention, leakage test | Poor flow, insert leakage, loose insert |
| Capsule / shrink sleeve | Neck height, shoulder transition, clearance | Shrink test, visual alignment, opening test | Wrinkles, blocked opening, poor finish |
This table shows why the bottle and closure should be reviewed as one packaging system, not as separate purchasing items.
Which Closure Type Should You Choose?
A private mold bottle project should start with the brand position, filling method, market requirement, and user experience. The closure should support the bottle design, not fight against it.
| Buyer Situation | Recommended Closure Direction |
|---|---|
| Premium whisky, rum, tequila, or brandy | Bar-top stopper or synthetic bar-top stopper |
| Vodka, gin, liqueur, RTD spirits, or export spirits | ROPP closure or screw cap |
| Anti-counterfeit or refill-control market | Non-refillable closure |
| Mini bottles or high-speed filling | Screw cap or ROPP cap |
| Strong premium shelf presentation | Bar-top stopper with capsule, sleeve, or decorative neck cover |
| Cost-sensitive private label project | Standard screw cap or standard synthetic stopper |
| Custom bottle with unusual bore or neck profile | Custom stopper shank, adjusted liner, or fit-tested closure system |
This decision table is only an early guide. Final approval should still be based on bottle drawings, physical samples, fit testing, and filling-line requirements.
How Different Closure Types Match Private Mold Bottles
Bar-Top Stoppers
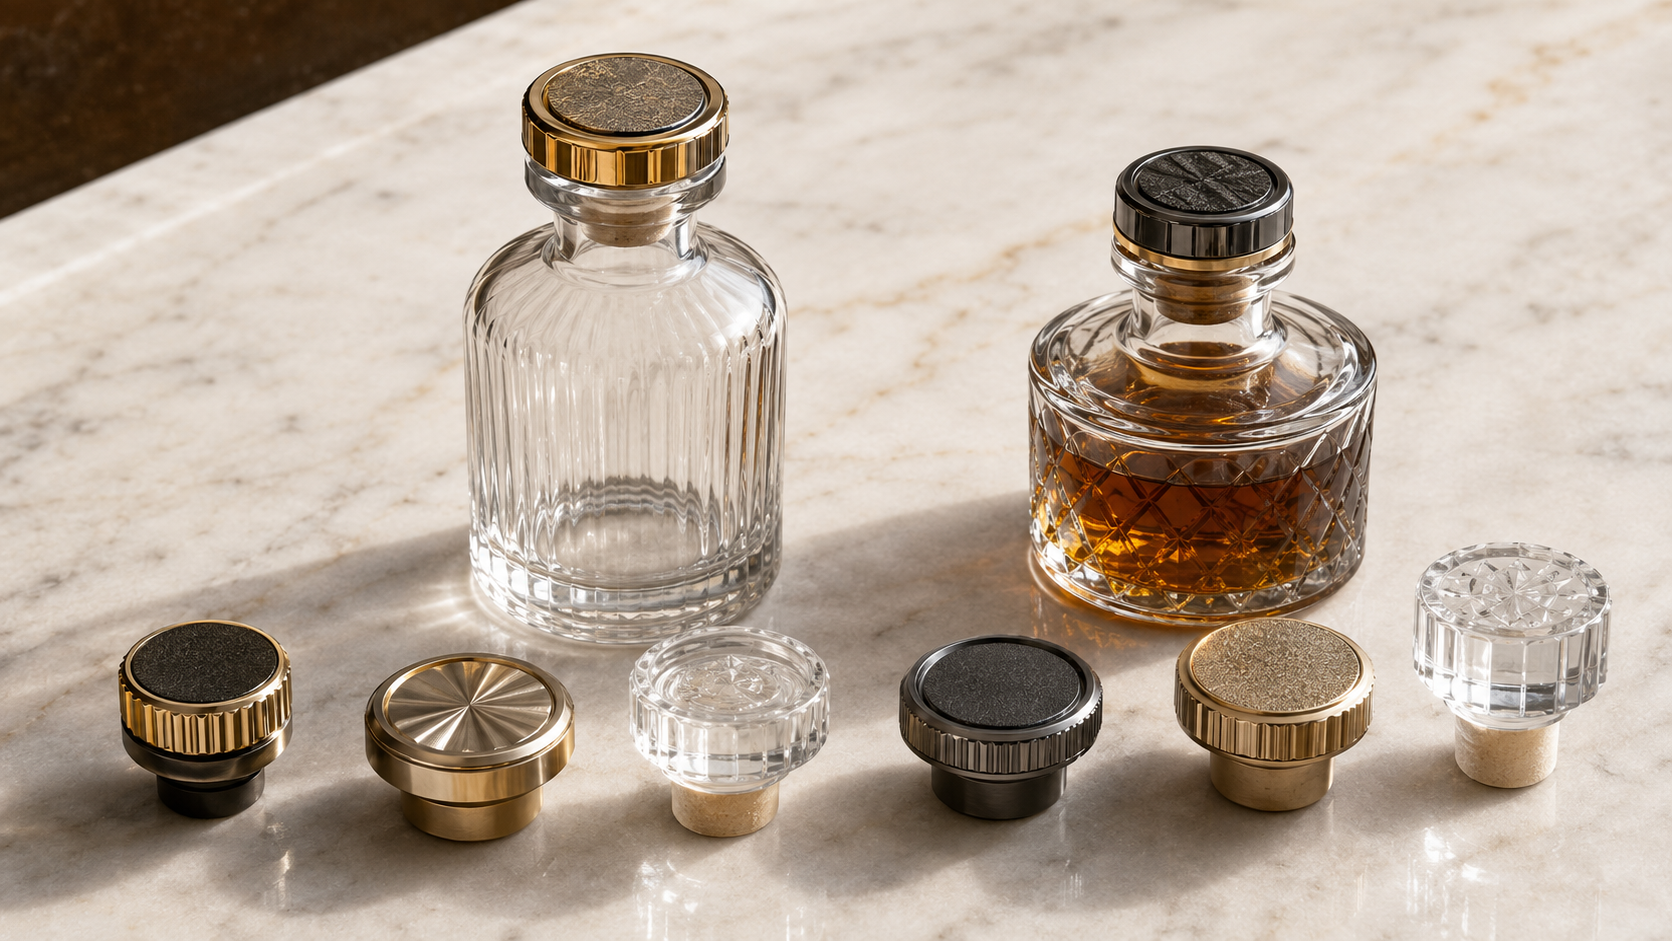
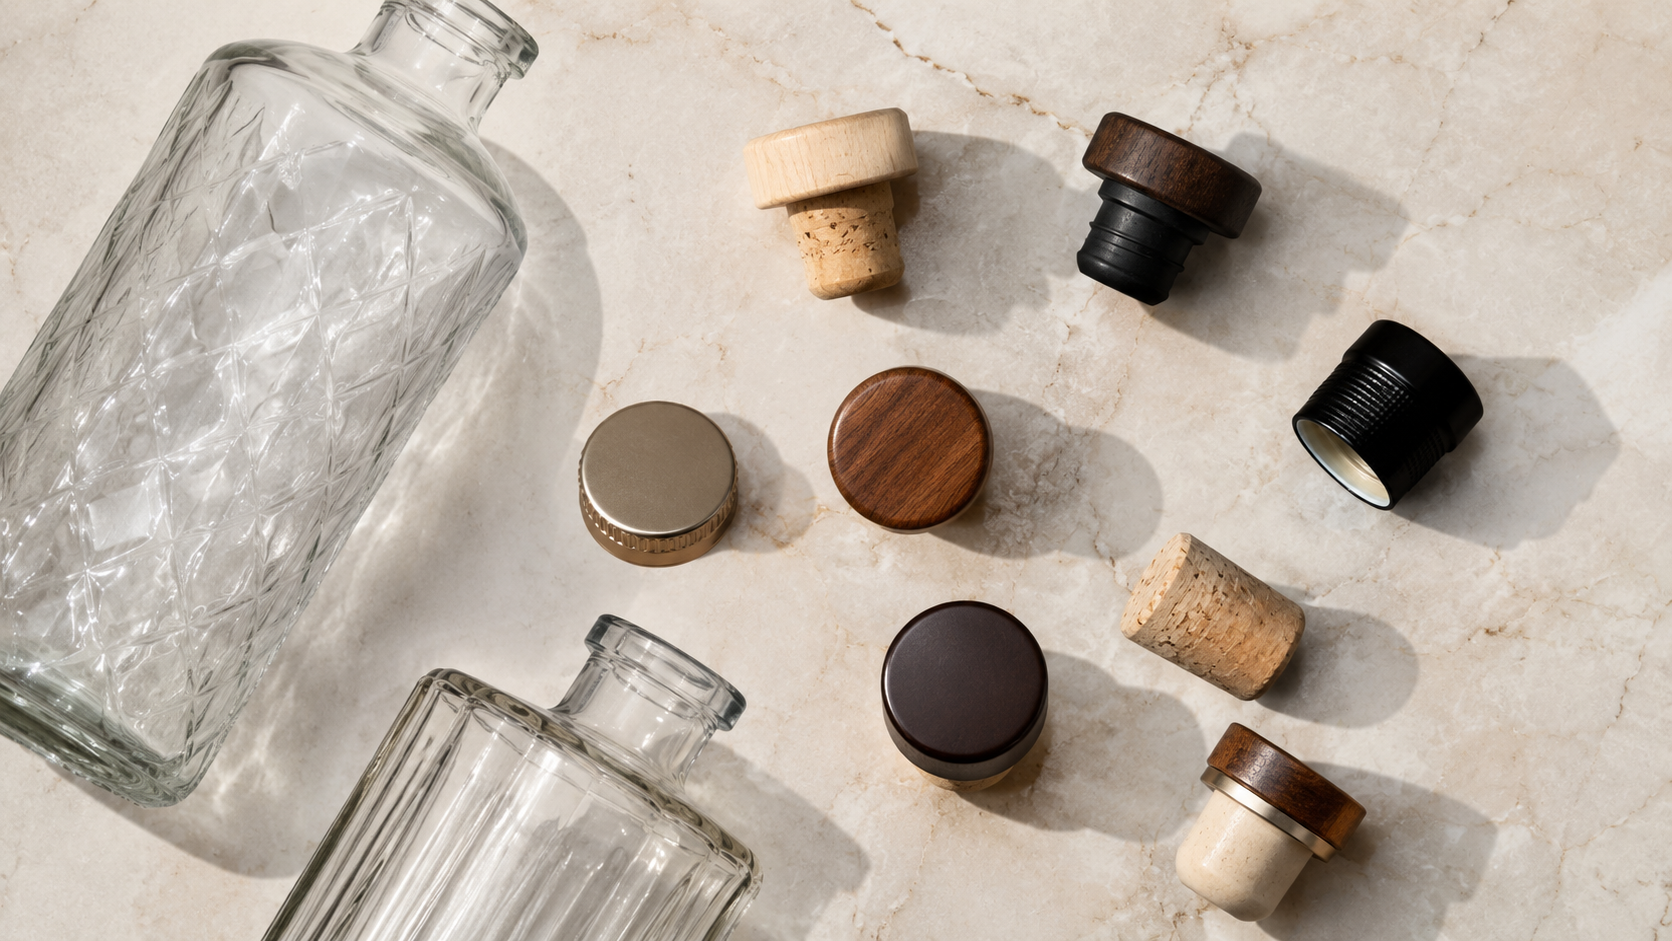
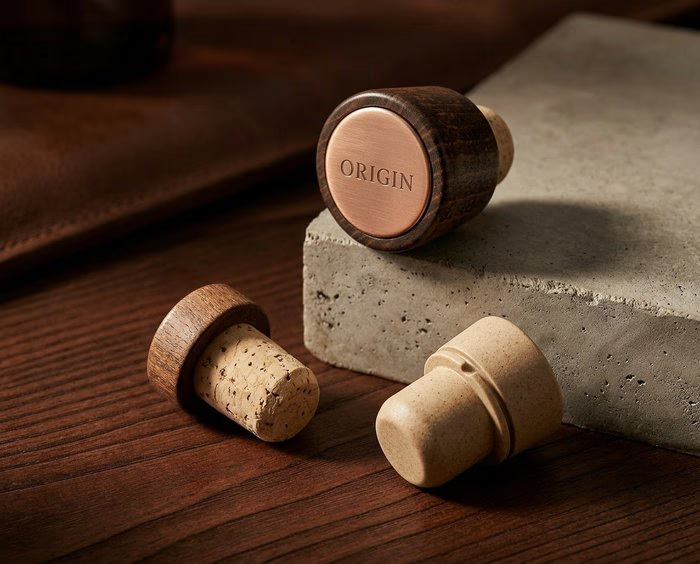
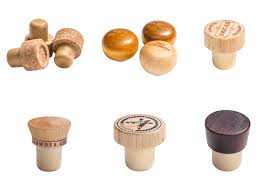
Bar-top stoppers are widely used for whisky, rum, tequila, gin, brandy, liqueur, and premium craft spirits. They combine a visible decorative top with an inserted shank.
For private mold spirits bottles, the most important fit factors are inner bore, bore tolerance, shank diameter, shank length, insertion depth, compression, pull-out force, resealing feel, and stopper top weight.
A common starting point is to make the stopper shank slightly larger than the bottle bore, but this should not be treated as the final rule. The final fit depends on material recovery, bore shape, storage conditions, and actual sample testing.
Kandacork supplies custom bar-top stoppers for spirits bottles with multiple top materials, shank options, logo processes, and bottle-fit support.
Synthetic Bar-Top Stoppers
Synthetic stoppers are useful when brands need controlled sizing, consistent color, modern appearance, and repeatable performance. They are often used for vodka, gin, tequila, rum, liqueur, and private label spirits.
For private mold bottles, synthetic shanks can often be adjusted based on the bottle drawing and sample test result. Buyers should still confirm insertion feel, pull-out resistance, sealing behavior, and long-term recovery before bulk production.
For bar-top stopper projects, Kandacork does not rely on bore size alone. The review should include bore tolerance, shank material, insertion depth, pull-out feel, resealing behavior, and storage conditions. For a deeper comparison, review this guide on cork shank vs synthetic shank for bar-top stoppers.
Screw Caps
Screw caps are used for spirits, mini bottles, liqueurs, RTD cocktails, and other beverage formats where resealability and production efficiency matter.
A screw cap must match the thread finish, cap height, liner, sealing land, and torque requirement. A cap may screw onto the bottle but still leak if the liner does not compress correctly or if the thread engagement is unstable.
For private mold bottles, screw cap testing should include application torque, removal torque, leakage review, liner contact, and visual alignment.
ROPP Closures
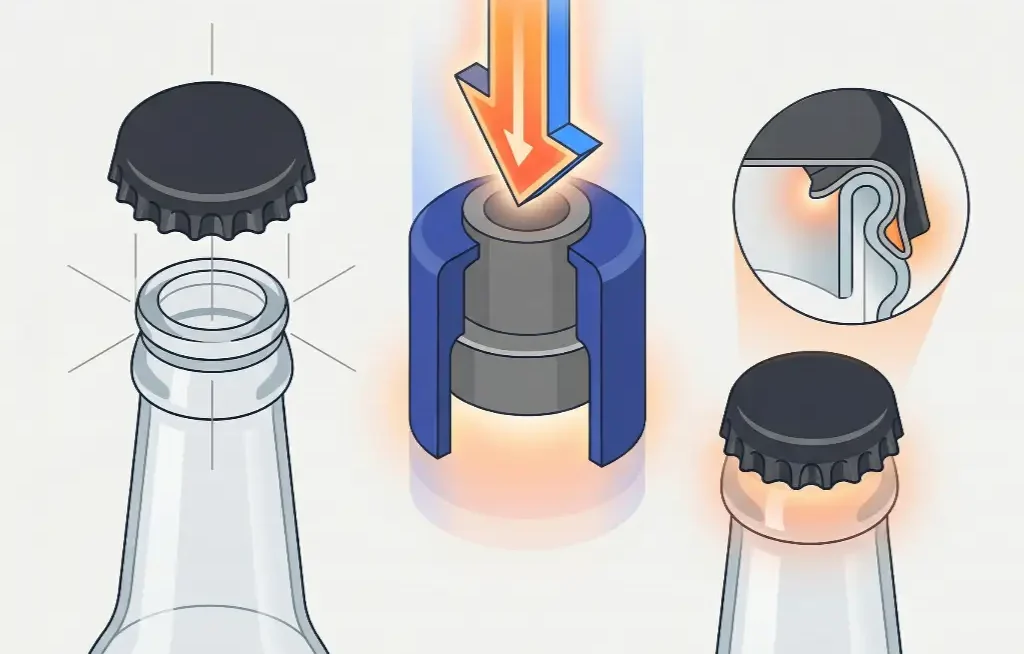
ROPP means roll-on pilfer-proof. ROPP closures are common for spirits projects that require aluminum presentation, tamper evidence, and machine application.
Unlike ordinary screw caps, ROPP caps are formed onto the bottle neck during capping. This means the bottle needs a suitable ROPP neck finish. The cap shell, liner, skirt height, pilfer band, and capping head setup must work together.
ROPP closure testing should include cap forming, bridge break, opening torque, tamper-band performance, and leakage review. Buyers comparing anti-refill and roll-on systems can also review Kandacork’s guide to non-refillable closures vs ROPP closures.
Non-Refillable Closures
Non-refillable closures are used for spirits projects that need pour control, anti-refill protection, export market support, or anti-counterfeit value.
These closures may include internal inserts, valves, pourers, or special sealing structures. Compatibility depends on bore shape, insert seating, pour path, closure stability, and leakage resistance.
Because non-refillable closures include internal components, physical bottle testing is especially important.
Capsules, Shrink Sleeves, and Decorative Neck Covers
Capsules, shrink sleeves, wax, foil, and decorative neck covers can improve premium appearance, but they may also affect closure function.
For private mold spirits bottles, buyers should check neck height, shoulder transition, clearance, shrink behavior, opening feel, and tamper-evident presentation before final approval.
Common Compatibility Failures in Private Mold Bottle Projects
1. The Bottle Mold Is Approved Before Closure Selection
This is one of the most expensive mistakes. The bottle design is approved first, and the buyer searches for a closure later. If the bore, thread, finish height, or sealing land is wrong, the closure supplier may need to change the stopper size, liner, cap structure, or recommend a different closure type.
2. The Drawing and Real Glass Sample Do Not Match Perfectly
A technical drawing is necessary, but it is not enough. Real glass samples may vary because of mold tolerance, production conditions, and finish control. Buyers should test closures on physical bottle samples before confirming bulk production.
3. The Closure Looks Correct but Fails Functionally
A stopper can look premium but feel loose after storage. A screw cap can thread onto the bottle but leak. An ROPP cap can look aligned but fail during application. A non-refillable insert can appear correct but pour poorly.
This is why appearance approval and functional approval should be separated during sampling.
4. Decoration Interferes With Fit
Thick coating, wax, foil, capsule, shrink sleeve, embossing, or an oversized stopper top can affect clearance, opening, closing, or tamper evidence. Decoration should be reviewed together with the closure, not added after compatibility testing is complete.
Closure Fit Problem Diagnosis
When a closure fails, the visible problem is often only a symptom. Buyers should diagnose the bottle neck, closure structure, material, and application process together.
| Problem | Possible Cause | What to Check |
|---|---|---|
| Stopper feels loose | Bore too large, shank too small, poor material recovery | Inner bore, shank diameter, pull-out force, storage test |
| Stopper is too hard to insert | Bore too small, shank too hard, insertion depth too long | Bore tolerance, shank hardness, insertion force |
| Screw cap leaks | Poor liner compression, uneven sealing land, wrong torque | Sealing land, liner material, application torque |
| Screw cap cross-threads | Thread mismatch or unstable thread engagement | Thread profile, S dimension, cap thread structure |
| ROPP cap spins | Wrong ROPP finish, poor forming, capper setup issue | Neck finish, skirt height, capping head setup |
| Tamper band breaks poorly | Wrong pilfer band area or bridge design | Band position, cap bridge, ROPP bead |
| Non-refillable insert leaks | Insert does not seat correctly inside the bore | Bore shape, insert size, sealing contact |
| Sleeve wrinkles | Neck or shoulder transition does not match sleeve design | Sleeve size, shrink ratio, shoulder profile |
This table can help packaging buyers prepare clearer feedback when sending samples back to the closure supplier.
How to Test Cap and Neck Compatibility Before Bulk Production
Step 1: Review the Bottle Drawing
Start with the technical drawing. It should include bottle capacity, total height, neck finish, inner bore, finish height, thread profile, sealing land, shoulder transition, fill level, and decoration area.
If the bottle mold has not been opened yet, this is the best stage to prevent closure problems. Buyers who need more background on bore and shank behavior can also read Kandacork’s article on how bar-top stoppers fit spirits bottle necks.
Step 2: Confirm the Closure Direction
Decide whether the project needs a bar-top stopper, synthetic stopper, screw cap, ROPP closure, non-refillable closure, capsule, shrink sleeve, or a combined closure system.
The closure direction should match the spirit type, brand position, filling method, destination market, opening experience, and tamper-evident requirement.
Step 3: Match Materials and Contact Points
For bar-top stoppers, review shank diameter, shank length, compression, and pull-out resistance.
For screw caps, review thread fit, liner contact, torque, and sealing land.
For ROPP closures, review cap forming, pilfer band area, and capping equipment.
For non-refillable closures, review insert fit, pour control, and leakage risk.
Step 4: Produce Functional Samples
A sample should represent the real production structure. A decorative sample is not enough if the final shank, liner, thread, insert, or cap material will be different.
Buyers should test the actual closure on the actual bottle whenever possible.
Step 5: Conduct Performance Testing
Testing does not need to be complicated at the first stage, but it should answer one question clearly: can this closure work reliably on this bottle in real production and transport conditions?
| Test | Applies To | What to Confirm |
|---|---|---|
| Visual fit review | All closures | Closure sits straight, no visible gap, tilt, or uneven contact |
| Pull-out test | Bar-top and synthetic stoppers | Secure grip, acceptable opening feel, stable resealing |
| Torque test | Screw caps and ROPP closures | Stable application torque and removal torque |
| Leakage test | All sealing closures | No leakage under defined storage or handling conditions |
| Inverted bottle test | Export spirits projects | No seepage after the agreed test period |
| Cap forming test | ROPP closures | Clean skirt forming, stable bridge break, no spinning |
| Insert retention test | Non-refillable closures | Insert stays secure and pours correctly |
| Packing review | Export projects | No abrasion, deformation, carton damage, or mixed-part risk |
Step 6: Approve the Complete Packaging System
Do not approve the bottle, closure, decoration, and carton separately. The final approval sample should include the actual bottle, actual closure, actual liner or shank, actual logo, actual capsule or sleeve if used, and final packing method.
This approved sample should become the reference for bulk production, inspection, and shipment.
RFQ Checklist: What to Send for Private Mold Bottle Closure Review
A complete RFQ helps the closure supplier recommend the right option faster and reduces repeated sampling rounds.
| RFQ Item | Why It Matters |
|---|---|
| Bottle drawing | Allows technical review before mold or sample approval |
| Neck finish detail | Helps match cap thread, ROPP finish, stopper structure, or insert fit |
| Inner bore size | Critical for bar-top stoppers, synthetic shanks, inserts, and pourers |
| Bottle sample | Confirms real fit beyond drawing data |
| Closure type | Defines whether the project needs stopper, screw cap, ROPP, or non-refillable closure |
| Material preference | Affects appearance, cost, performance, and brand positioning |
| Logo requirement | Determines printing, embossing, engraving, debossing, or other branding method |
| Spirit type and ABV | Helps assess sealing, material contact, and storage conditions |
| Filling method | Affects torque, application speed, and closure structure |
| Tamper-evident need | Important for export markets and regulatory requirements |
| Estimated quantity | Supports quotation, MOQ, and production planning |
| Destination market | Helps review compliance, packing, and shipping requirements |
| Target launch date | Helps plan sampling, testing, production, and shipment |
Buyers who can provide drawings, samples, quantity, and project requirements will usually receive more accurate sample recommendations and quotations.
To move from technical review to pricing, send Kandacork your bottle drawing, neck finish detail, closure idea, estimated quantity, and destination market for sample or quotation support.
How to Choose a Closure Supplier for Private Mold Bottle Projects
A private mold bottle project needs more than a standard cap supplier. Buyers should look for a closure partner that can support technical review, sampling, testing, decoration, production, and export packaging.
1. Can the Supplier Review Bottle Drawings Before Mold Approval?
A capable supplier should understand neck finish, inner bore, thread structure, sealing land, stopper shank fit, liner contact, cap height, and application method.
2. Can the Supplier Test Real Bottle Samples?
Physical testing is important because actual glass samples may differ from drawings. The supplier should be able to test closures on buyer-provided bottle samples before bulk confirmation.
3. Can the Supplier Support Multiple Closure Types?
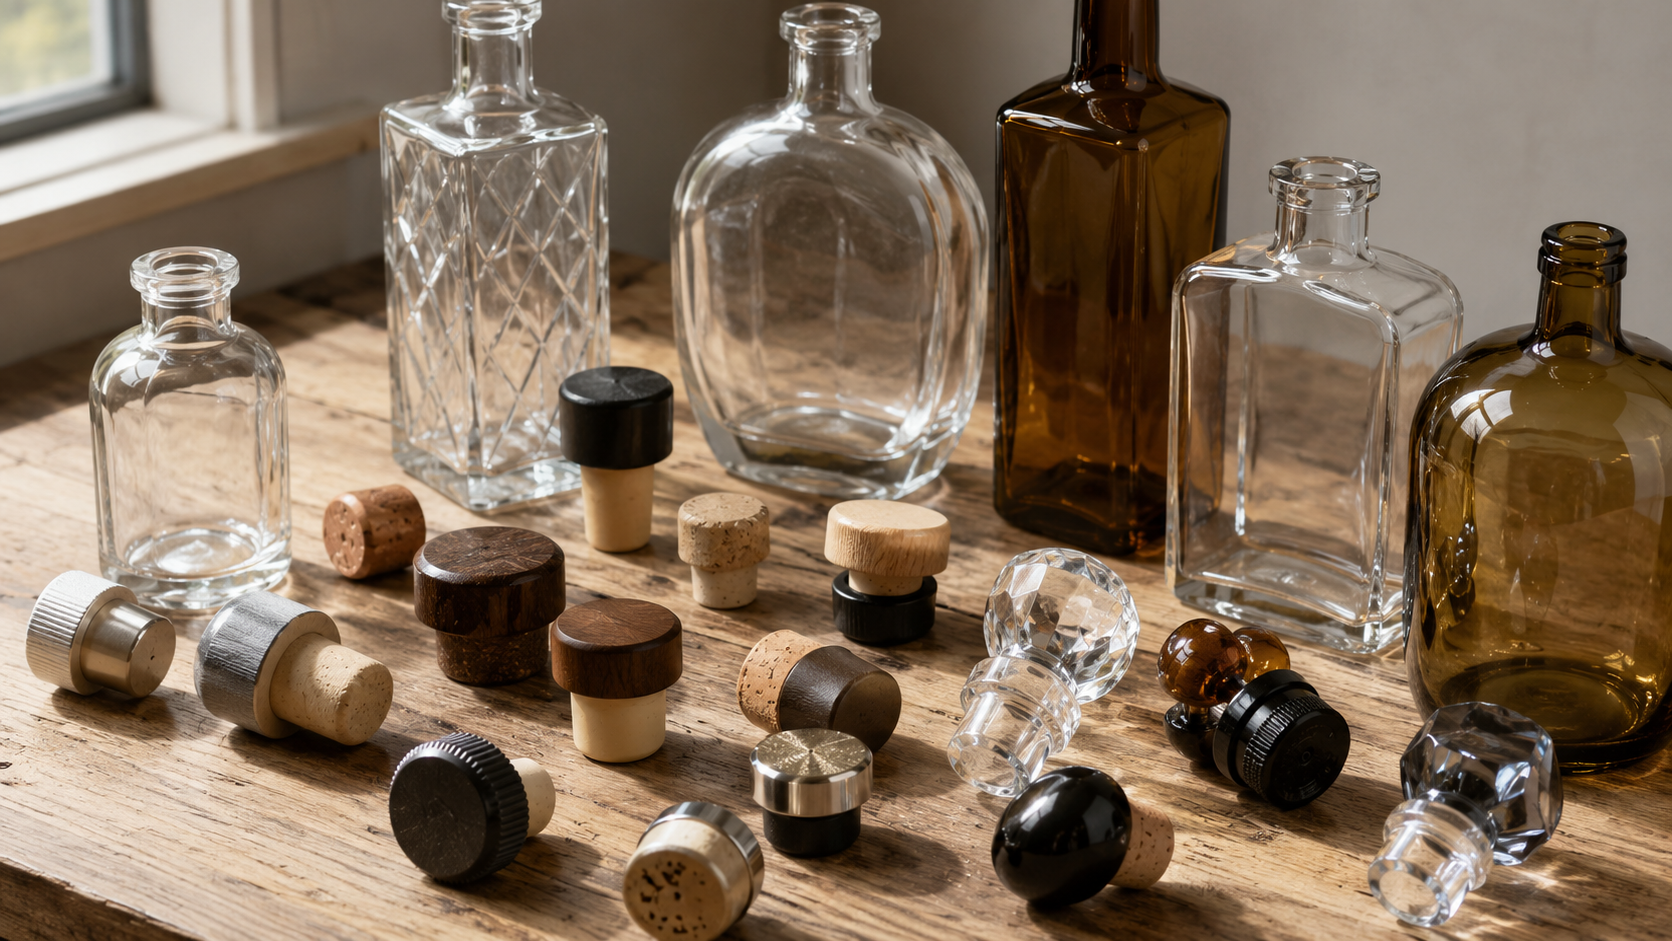
Private mold spirits bottles may require bar-top stoppers, synthetic stoppers, wooden stoppers, screw caps, ROPP closures, non-refillable closures, capsules, or shrink sleeves.
A supplier with a wider closure range can compare solutions instead of forcing one standard option.
4. Can the Supplier Adjust Fit and Decoration?
For custom projects, the supplier should be able to adjust stopper shank size, liner selection, cap height, surface finish, color, logo method, and decoration process based on the bottle and brand requirements.
5. Can the Supplier Support Testing and Export Packing?
Fit testing alone is not enough. The supplier should also consider leakage, torque, pull-out resistance, tamper evidence, appearance quality, carton protection, labeling, and export shipment conditions.
Kandacork Closures & Stoppers supports spirits brands with custom bar-top stoppers, synthetic stoppers, screw caps, ROPP closures, capsules, shrink sleeves, neck-fit review, logo decoration, sampling, quality testing, and export-ready bulk supply.
FAQ
What is cap and neck compatibility for private mold bottles?
It is the process of matching the bottle neck finish, inner bore, sealing surface, thread profile, and closure structure before sampling or bulk production. For private mold bottles, this reduces leakage, fit failure, and mold correction risk.
How do I know which cap fits my bottle neck?
You need to confirm more than the diameter. Check the neck finish, thread style, T dimension, E dimension, I dimension, H dimension, sealing land, liner contact, and closure application method.
Can I use a standard cap on a private mold spirits bottle?
Sometimes. A standard cap can work if the private mold bottle follows a compatible neck finish and tolerance. However, it should still be tested on real bottle samples before bulk approval.
What neck dimensions are needed for bar-top stoppers?
The most important dimension is the inner bore. Buyers should also confirm bore tolerance, insertion depth, stopper shank diameter, shank material, and pull-out resistance.
What is the difference between CT screw caps and ROPP closures?
CT screw caps are threaded closures that screw onto a matching bottle finish. ROPP closures are aluminum caps formed onto the bottle neck during capping and require a suitable ROPP neck finish.
What should I send to Kandacork for quotation?
Send your bottle drawing, neck finish detail, inner bore size, bottle sample if available, closure idea, spirit type, ABV, filling method, destination market, logo requirement, estimated quantity, and target launch date.